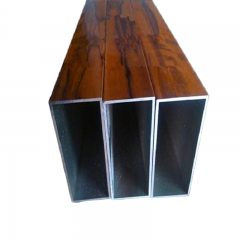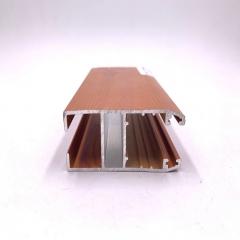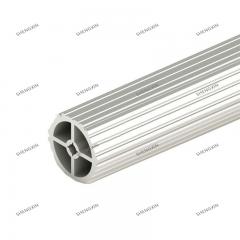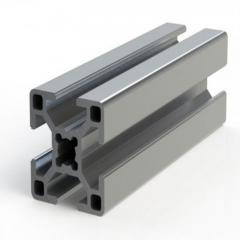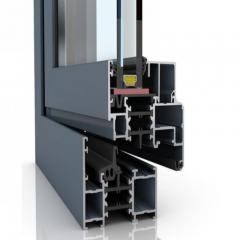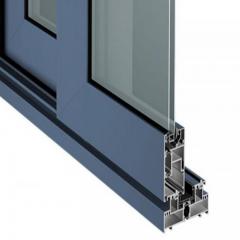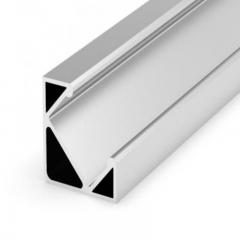
Ever wondered how engineers create those incredibly precise aluminum frames supporting everything from factory automation systems to architectural facades? The answer lies in structural aluminum extrusion profiles—engineered components designed specifically to bear loads, resist deformation, and form the backbone of countless industrial and construction applications.
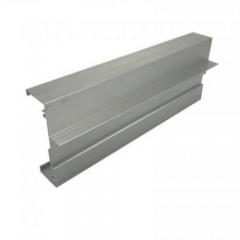
Structural aluminum extrusion profiles are load-bearing aluminum shapes produced by forcing heated aluminum alloy through precision dies, creating consistent cross-sectional geometries engineered to meet specific mechanical performance requirements for frames, supports, and assemblies.
So what is aluminum extrusion, exactly? Picture pushing modeling clay through a shaped opening—that's the basic principle, scaled up dramatically with sophisticated engineering. The aluminum extrusion process begins with cylindrical aluminum billets, typically heated to temperatures between 750 and 900 degrees Fahrenheit. At this temperature, the aluminum becomes malleable but remains solid, allowing it to flow through steel dies under immense hydraulic pressure—sometimes exceeding 15,000 tons of force.
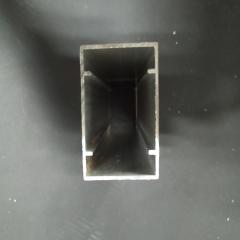
As the heated billet is forced through the die opening, it emerges on the other side with a cross-sectional shape that precisely matches the die's design. This extrusion of aluminium can produce profiles ranging from simple solid bars to complex hollow shapes with multiple internal voids. The beauty of this process? Every inch of the extruded profile maintains the exact same cross-section, delivering remarkable consistency that machining or fabrication simply cannot match economically.
What transforms ordinary aluminum extruded material into true structural-grade profiles? It comes down to three critical factors working together:
According to the Aluminum Extruders Council's Extrusion Manual, appropriately alloyed aluminum can reach ultimate tensile strengths as high as 90,000 PSI, approaching those of steel while weighing only one-third as much.
Not all aluminum extrusion profiles serve the same purpose. Decorative trim pieces, window frames, and general-purpose shapes may share the same manufacturing process, but structural profiles are engineered with fundamentally different priorities.
Decorative extrusions prioritize surface finish, intricate detailing, and visual appeal. Structural profiles, by contrast, are designed around mechanical performance—tensile strength, yield strength, moment of inertia, and fatigue resistance. When you're building machine frames, safety guarding, or architectural support structures, these engineering properties matter far more than aesthetic considerations.
The distinction also extends to quality control. Structural aluminum extrusions undergo more rigorous testing and must meet tighter dimensional tolerances, particularly for features that affect load distribution and connection integrity. This ensures that when engineers specify structural profiles for critical applications, the delivered products will perform exactly as calculated.
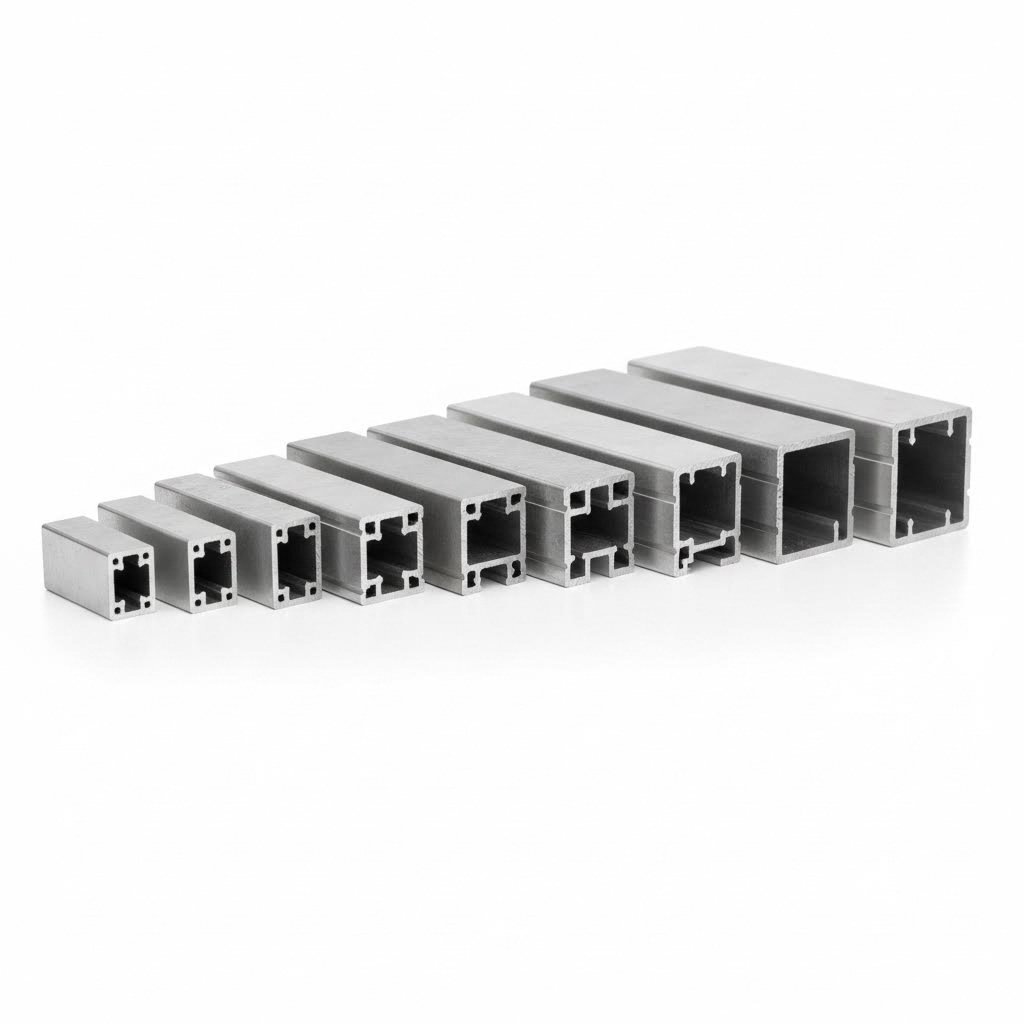
Now that you understand what makes aluminum profiles structural grade, you're probably wondering: how do you actually choose the right size for your project? Walk into the world of aluminum t slot systems, and you'll immediately encounter numbers like 10, 15, 20, 40, or even 80 series. These aren't random—they're the key to matching profile strength with your application's demands.
Here's what those series numbers actually mean. According to 80/20's naming convention guide, the series number represents the broader category based on general profile size. For fractional (imperial) series, the number typically corresponds to the profile's base dimension in inches multiplied by ten. For metric series, the number directly indicates the profile's base dimension in millimeters.
Sounds complex? Think of it this way: a 10 series profile measures approximately 1 inch (25.4mm) square, while a 40 series profile measures 40mm square. The t slot rail width also scales proportionally—larger series profiles have wider slots that accept correspondingly larger fasteners capable of handling greater loads.
The naming convention typically follows this pattern: [Series Number]-[Profile Size]x[Profile Size/Shape]-[Additional Features]. So when you see "4040" on a spec sheet, you're looking at a 40 series profile with 40mm x 40mm dimensions—a common choice in t slotted framing for industrial applications.
Each series offers distinct advantages depending on your structural requirements. Here's how the major series break down:
| Series | Typical Dimensions | Slot Width | Load Capacity | Best Applications |
|---|---|---|---|---|
| 10 Series | 1" x 1" (25.4mm) | Narrow | Light-duty | Displays, lightweight enclosures, workstations |
| 15 Series | 1.5" x 1.5" (38.1mm) | Medium | Medium-duty | Automation frameworks, machine bases |
| 20 Series | 20mm x 20mm | Narrow | Light-duty | Small projects, space-constrained applications |
| 25 Series | 25mm x 25mm | Narrow-Medium | Moderate | Medium enclosures, test fixtures |
| 30 Series | 30mm x 30mm | Medium | Medium-duty | Automation, test rigs, moderate load structures |
| 40 Series | 40mm x 40mm | Wide | Heavy-duty | Industrial machine frames, large enclosures |
| 45 Series | 45mm x 45mm | Wide | Heavy-duty | Heavy machinery, structural applications |
| 80 Series | 80mm x 80mm | Extra-wide | Maximum | Large spans, heavy industrial equipment |
When evaluating 80/20 aluminum or similar tslots systems, remember that the series you select determines which connectors, fasteners, and accessories you can use. As CPI Automation notes, sticking with a specific series throughout your project ensures consistency and avoids compatibility headaches.
Choosing the right series involves balancing four key factors:
Imagine you're building a workstation frame with a desktop surface spanning 36 inches. For light office use, a 15 series might suffice. But add CNC equipment weighing 200 pounds? You'll want 40 series profiles to prevent deflection and ensure long-term stability. Need that same frame to support robotic welding equipment? Now you're looking at 80 series profiles or engineered reinforcement strategies.
The 15 series has become particularly popular among 8020 aluminum extrusion users because it strikes an excellent balance between versatility and cost-effectiveness—strong enough for most automation and light industrial applications while remaining economical for larger projects.
Understanding these sizing fundamentals prepares you for the next critical decision: selecting the right aluminum alloy and temper combination to deliver the mechanical properties your application demands.
You've selected the right profile series for your project dimensions—but here's where many engineers hit a wall. Those cryptic codes like 6063-T5 or 6061-T6 stamped on every aluminum extrusion profile aren't just manufacturer jargon. They determine whether your structure will perform flawlessly for decades or fail under stress. Understanding these designations is the difference between over-engineering (wasting money) and under-engineering (risking failure).
When you see a four-digit number like 6061 or 6063, you're looking at the aluminum alloy designation system. The first digit identifies the primary alloying element—for structural aluminium extrusion applications, you'll almost exclusively encounter 6xxx series alloys, where magnesium and silicon are the key additions.
Why does this matter? These alloying elements enable heat treatment, which dramatically increases strength after extrusion. Here's what the three primary structural alloys bring to the table:
Each aluminum profile type serves distinct purposes. When you need intricate shapes with anodized aluminum finishes for architectural facades, 6063 delivers. When structural demands require maximum strength and the profile will be machined afterward, 6061 becomes the clear choice.
The letter and number following the alloy—like the T5 in 6063-T5—tells you exactly how the material was processed after extrusion. This temper designation dramatically affects mechanical properties.
The "T" indicates thermal treatment, and the following number specifies the exact process:
Here's what these temper differences mean in practice: 6063-T5 might yield at 21,000 PSI, while 6063-T6 reaches 31,000 PSI—a 48% strength increase from the same base alloy. However, T6 processing adds cost and lead time, so specifying it unnecessarily wastes budget.
This decision comes up constantly when specifying types of extruded aluminum for structural applications. The following comparison breaks down what actually matters:
| Property | 6063-T5 | 6063-T6 | 6061-T6 | 6005-T5 |
|---|---|---|---|---|
| Yield Strength (PSI) | 21,000 | 31,000 | 40,000 | 35,000 |
| Tensile Strength (PSI) | 27,000 | 35,000 | 45,000 | 38,000 |
| Elongation (%) | 12 | 12 | 12 | 10 |
| Extrudability | Excellent | Excellent | Fair | Good |
| Surface Finish | Excellent | Excellent | Good | Good |
| Weldability | Good | Good | Good | Good |
| Corrosion Resistance | Excellent | Excellent | Good | Excellent |
| Machinability | Fair | Fair | Excellent | Good |
| Typical Applications | Architectural, modular framing | Higher-load framing | Machine parts, heavy structures | Transportation, bridges |
Notice the weldability row? All 6xxx alloys weld reasonably well, but here's the catch—welding creates a heat-affected zone that reduces strength by 30-50% near the weld. For extruded aluminium structures requiring maximum integrity, mechanical fastening or specialized welding techniques with post-weld heat treatment become necessary.
When selecting your alloy and temper, ask these questions:
For most modular T-slot framing systems, 6063-T5 or 6063-T6 delivers the best balance of performance, availability, and cost. When you're designing custom structural components facing heavy loads or requiring extensive secondary machining, 6061-T6 justifies its premium. Understanding these distinctions ensures you're specifying exactly what your application needs—nothing more, nothing less.
With alloy and temper selection clarified, you're ready to explore the fundamental choice between modular T-slot systems and traditional structural shapes—each offering distinct advantages depending on your assembly and reconfiguration requirements.
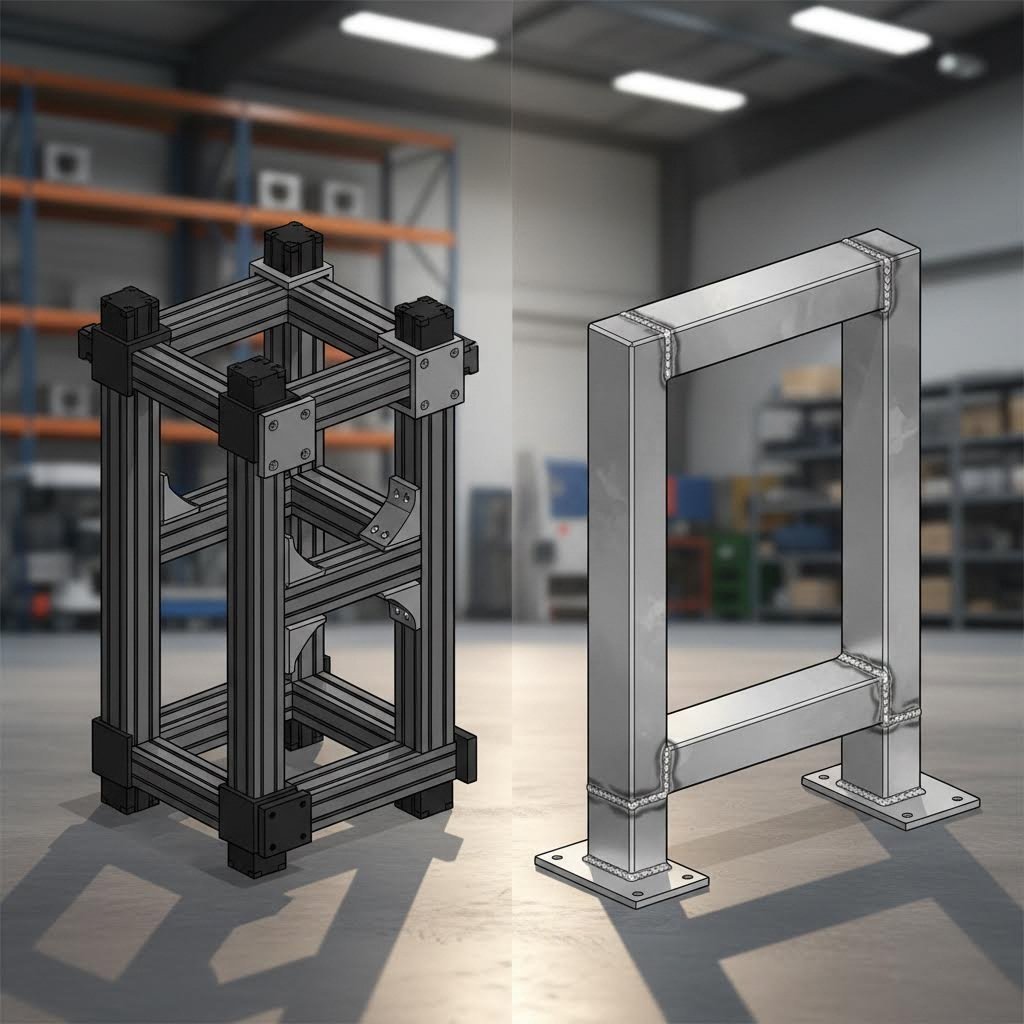
You've nailed down your alloy selection and profile sizing—now comes a fundamental choice that shapes your entire project approach. Should you build with modular t slotted aluminum extrusions that bolt together like an industrial erector set? Or go with traditional aluminum shapes that require welding or permanent fasteners? Each path leads to successful structures, but the journey looks completely different.
Think of T-slotted profiles as a building system rather than just raw material. Every extruded aluminum framing piece features continuous grooves running along its length—these T-shaped channels accept specialized fasteners that slide in and lock anywhere along the profile. No drilling. No welding. Just position and tighten.
Traditional structural shapes—aluminum angle, aluminum tubing, channels, and I-beams—take the opposite approach. These standard shapes offer straightforward geometry optimized for specific loading conditions, but joining them requires either welding or drilling through the material for mechanical fasteners. Once assembled, the structure stays put.
The aluminum extrusion shapes you choose fundamentally determine your assembly process, modification flexibility, and total project cost. Here's what each approach actually delivers:
Imagine building a workstation for electronics assembly. Operators need adjustable shelving, monitor mounts that move, and tool holders positioned exactly where they're most efficient. Six months later, the product changes and the entire layout needs reconfiguring. With extruded aluminum shapes in a T-slot system, you'll spend an afternoon making adjustments. With welded aluminum tubing, you're cutting apart the old frame and starting over.
Now picture a permanent machine base supporting a 5,000-pound CNC mill. This structure never needs modification—it needs absolute rigidity and maximum load capacity. Here, welded aluminum shapes or heavy-duty structural sections make far more sense than modular framing.
The decision often comes down to asking: will this structure need to change during its service life?
Different applications naturally favor one approach over the other. Here's how common projects typically align:
Many successful projects actually combine both approaches—using T-slotted profiles for adjustable workstation elements mounted to welded structural bases for maximum rigidity. Understanding when to use each system, and how they complement each other, gives you the flexibility to optimize every aspect of your design.
Once you've determined your profile type, the next challenge becomes matching specific profiles to your application's unique requirements—load types, spans, environmental conditions, and the real-world demands your structure will face daily.
You've chosen between modular and traditional profiles—but here's where the rubber meets the road. Picking the right aluminum extrusion frame for your specific application requires thinking like an engineer, not a catalog shopper. What loads will your structure face? How far must profiles span without support? Will it sit in a climate-controlled office or a corrosive wash-down environment? Let's break down the selection process by what actually matters: your application.
Machine frames represent the most demanding application category for aluminum structural framing. Your profile selection here directly affects equipment accuracy, vibration damping, and long-term dimensional stability.
When you're building frames for CNC equipment, robotic cells, or precision assembly machines, you'll encounter forces working in multiple directions simultaneously. A milling machine doesn't just push down—it creates torsional loads, side forces from cutting operations, and dynamic vibrations that compound over millions of cycles.
Use this checklist when selecting profiles for machine frames:
For heavy equipment bases, an extruded frame built from 80 series profiles often delivers the rigidity needed without resorting to steel construction. The weight savings alone can simplify installation and reduce floor loading requirements.
Workstation design flips the priority list. Here, adjustability and human factors trump maximum load capacity. Modular aluminum framing shines in this application because workers' needs change—new tools arrive, processes evolve, and ergonomic improvements require repositioning components.
Consider these selection factors for workstation structures:
For most workstation applications, 30 or 40 series profiles provide the ideal balance. They're strong enough for typical industrial loads while remaining cost-effective and visually unobtrusive. Aluminum extrusion frame kits designed specifically for workstations often bundle appropriately sized profiles with ergonomic accessories, simplifying specification.
Safety enclosures protect people from hazardous machinery—making profile selection a life-safety decision, not just an engineering preference. Regulatory requirements, impact resistance, and panel integration all influence your choices.
When specifying profiles for machine guarding:
Environmental conditions matter significantly for enclosures. A guard around wash-down equipment needs different surface treatment than one in a climate-controlled assembly area. Corrosive atmospheres, UV exposure, and temperature extremes all factor into both profile material selection and surface finish specification.
For typical safety guarding applications, 40 series profiles handle most requirements. Lighter 30 series works for smaller enclosures with limited span requirements, while 45 or 80 series becomes necessary for large perimeter guarding or high-impact applications.
Here's something many catalogs never mention: the same profile performs dramatically differently depending on how you orient it. Understanding load direction—compression, tension, bending, and torsion—helps you get maximum performance from every extrusion.
Consider a rectangular profile measuring 40mm x 80mm. Oriented with the 80mm dimension vertical, it resists bending loads excellently when force is applied from above. Rotate it 90 degrees, and bending resistance drops significantly—but lateral stiffness increases. Same profile, same cost, vastly different performance.
Apply these orientation principles:
This application-first thinking transforms profile selection from catalog browsing into genuine engineering. You're not just picking sizes—you're optimizing every component for its specific role in your structure. With these selection principles established, the next consideration becomes protecting your carefully chosen profiles through appropriate surface treatments that match your environmental conditions.
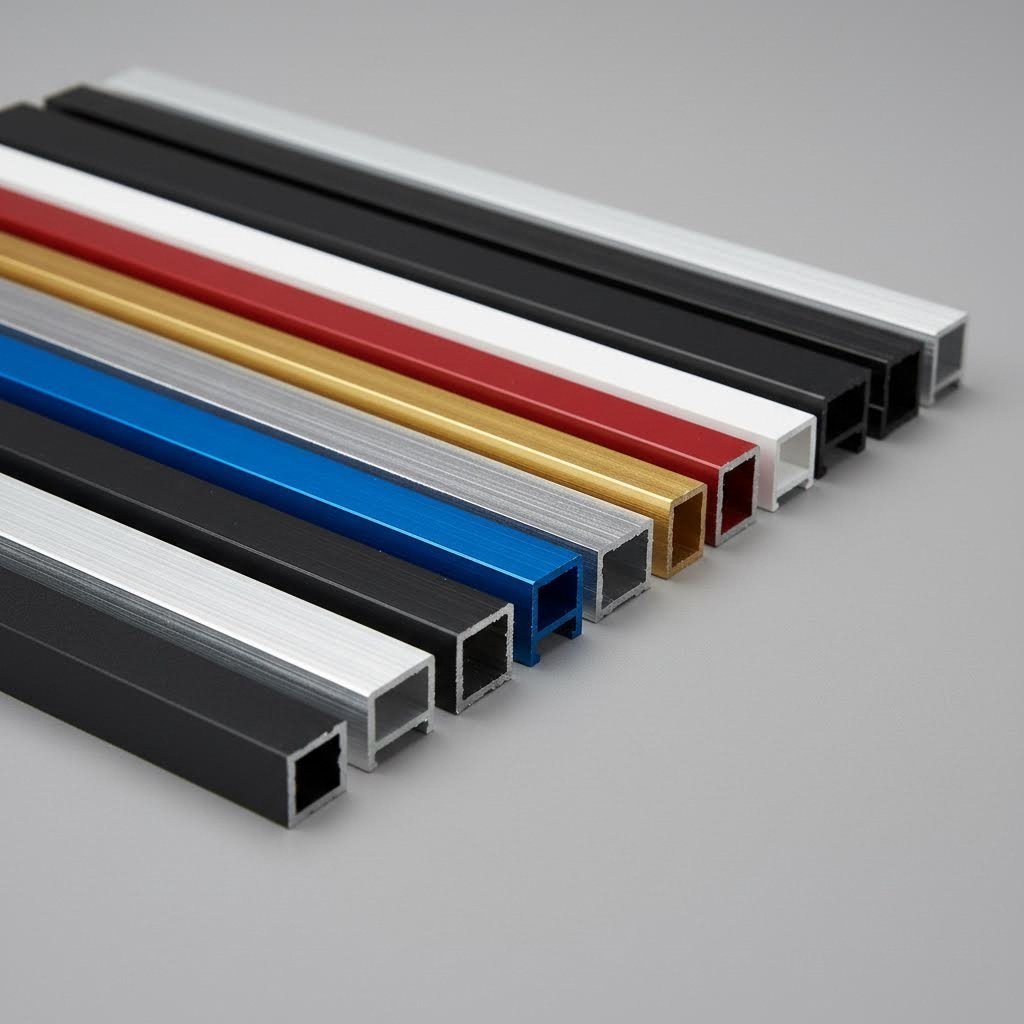
You've selected the perfect alloy, sized your profiles correctly, and optimized orientation for your loads—but here's what many engineers overlook until it's too late. That pristine aluminum surface you're admiring? Without proper treatment, it can degrade, discolor, or lose structural integrity depending on where your assembly lives and works. Surface treatments aren't just cosmetic upgrades—they're engineering decisions that affect performance, longevity, and even fastener compatibility.
When aluminum extrusions leave the press, they immediately begin forming a thin natural oxide layer. Anodizing takes this process and supercharges it, creating a controlled oxide coating that becomes part of the aluminum itself rather than sitting on top like paint.
Here's what happens during anodizing: your aluminium profile gets immersed in an electrolytic bath (typically sulfuric acid), and electrical current drives oxygen ions into the surface. The result? A hard, porous aluminum oxide layer that can be sealed for maximum protection or dyed for color before sealing.
Three anodizing types dominate structural applications:
Anodic layer thickness directly correlates with protection level. A standard 0.7 mil clear coat handles indoor environments excellently. Outdoor installations or corrosive atmospheres typically need 1.0 mil minimum. Hard-coat applications for wear resistance may specify 2.0 mils or more—though thicker coatings add cost and can affect dimensional tolerances on precision features.
When you need vibrant colors, thick protective layers, or specific aesthetic finishes that anodizing can't deliver, powder coating and PVDF coatings step in.
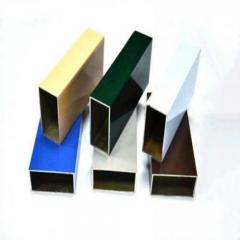
Powder coating electrostatically applies dry polymer particles to the aluminium extruded profile surface, then heat-cures them into a continuous film. The result is a durable finish 2 to 6 mils thick—significantly heavier than anodizing—available in virtually unlimited colors and textures including metallics, mattes, and textured finishes.
PVDF (polyvinylidene fluoride) coatings represent the premium tier for architectural aluminium profiles. These fluoropolymer finishes offer exceptional UV stability, color retention, and weathering resistance measured in decades rather than years. You'll find PVDF coatings specified on building facades, curtain walls, and exterior applications where appearance must remain consistent for 20+ years.
Consider your environment when choosing between these options:
Selecting surface treatments requires matching protection level to actual service conditions. Over-specifying wastes budget; under-specifying leads to premature failure.
| Treatment Type | Thickness Range | Durability | Color Options | Relative Cost | Best Applications |
|---|---|---|---|---|---|
| Clear Anodize (Type II) | 0.4-1.0 mils | Good | Natural aluminum only | Low | Indoor equipment, clean environments |
| Colored Anodize | 0.4-1.0 mils | Good | Limited palette | Low-Medium | Workstations, architectural interiors |
| Hard-Coat Anodize (Type III) | 1.0-4.0 mils | Excellent | Dark gray/black | Medium-High | Wear surfaces, sliding components |
| Powder Coating | 2.0-6.0 mils | Very Good | Unlimited | Medium | Enclosures, colored structures |
| PVDF Coating | 1.0-1.5 mils | Outstanding | Wide palette | High | Architectural exteriors, facades |
| Micro-Arc Oxidation | 1.0-8.0 mils | Exceptional | Limited | Very High | Extreme wear, thermal, or corrosive environments |
Don't overlook how surface treatment affects assembly. Anodized surfaces are electrically non-conductive—critical for grounding considerations but excellent for electrical isolation. Powder coating adds thickness that may require oversized holes or modified fastener specifications. Hard-coat anodizing's extreme hardness can make field modifications difficult without specialized tooling.
For demanding environments where standard treatments fall short, micro-arc oxidation (MAO) creates ceramic-like oxide layers with exceptional hardness, thermal resistance, and corrosion protection. This specialized process suits aerospace, military, and extreme industrial applications where profile aluminum faces conditions that would destroy conventional finishes.
Working with manufacturers offering comprehensive surface treatment capabilities—from standard anodizing through specialized processes like MAO—streamlines your supply chain and ensures treatment specifications align perfectly with your profile requirements. Shengxin Aluminium's deep processing services, for example, provide anodizing in custom colors, powder coating, PVDF, and micro-arc oxidation under one roof, eliminating coordination headaches between extrusion and finishing suppliers.
With surface protection specified, you're nearly ready to finalize your structural aluminum extrusion profiles—but one major decision remains: should you source standard catalog profiles or invest in custom extrusion development?
You've specified your alloy, sized your profiles, and selected surface treatments—but now comes a decision that affects everything from project timeline to long-term costs. Should you order extruded aluminum profiles straight from an aluminum extrusion profile catalog, or invest in custom die development for profiles engineered specifically for your application? This choice isn't as straightforward as it might seem, and getting it wrong can either waste budget on unnecessary custom tooling or force compromises that haunt your design for years.
Here's the truth most suppliers won't tell you: standard aluminum extrusions handle the vast majority of structural applications perfectly well. Before exploring custom options, honestly assess whether catalog profiles can do the job.
Standard profiles earn their place in your project when:
Think about it this way: decades of engineering refinement have shaped today's extruded aluminum sizes. Those 40 series T-slot profiles aren't arbitrary—they represent optimized solutions to common structural challenges. When your application fits within established parameters, standard profile extrusions deliver proven performance without reinventing the wheel.
The aluminum extrusion profiles catalog from any major supplier offers hundreds of cross-sections covering T-slots, angles, channels, tubes, and specialized shapes. Before assuming you need custom development, thoroughly explore what's already available. You might find that combining two standard profiles achieves your goals more economically than developing one custom shape.
When standard shapes genuinely can't meet your requirements, custom extrusion opens remarkable possibilities. Understanding the process helps you plan realistic timelines and budgets.
The journey from concept to custom profile follows these stages:
Custom profiles unlock capabilities impossible with standard shapes. Imagine integrating wire channels directly into your structural members—no separate conduit, no mounting hardware, just clean functionality. Or consider profiles with built-in mounting features for specific components, eliminating secondary machining operations. Thermal management fins, snap-fit panel grooves, and proprietary connection geometries all become possible when you control the cross-section.
The real power of custom extrusion emerges when you combine multiple functions into single profiles. A structural upright that also serves as a cable raceway, incorporates LED lighting channels, and provides precise panel alignment features might replace three or four separate components. This consolidation reduces assembly labor, minimizes hardware counts, and creates cleaner final products.
Custom dies represent fixed costs that must be amortized across production volume. Understanding where the economics shift helps you make informed decisions.
Consider this simplified comparison:
At these rates, the custom profile becomes more economical after approximately 3,600 linear feet—where tooling cost divided by per-foot savings equals break-even volume. Order less than that, and standard profiles cost less overall despite higher per-foot pricing.
But raw material cost tells only part of the story. Factor in these hidden economics:
For serious custom extrusion projects, comprehensive suppliers offering end-to-end support from die development through mass production streamline the entire process. Shengxin Aluminium's custom extrusion services maintain 35 extrusion presses ranging from 600T to 5500T capacity, enabling production of profiles from delicate architectural trim to heavy structural sections—all supported by in-house die design and CNC deep processing capabilities that eliminate coordination between multiple vendors.
When evaluating custom versus standard, don't let upfront die costs obscure total lifecycle economics. A $3,000 die investment that saves $0.50 per unit across a 50,000-unit production run represents $25,000 in savings—an 8:1 return on tooling investment. Run the numbers for your specific situation before defaulting to catalog selections.
Whether you source standard catalog profiles or develop custom solutions, your next challenge remains the same: assembling those profiles into rigid, reliable structures using appropriate fastening systems and connection methods.
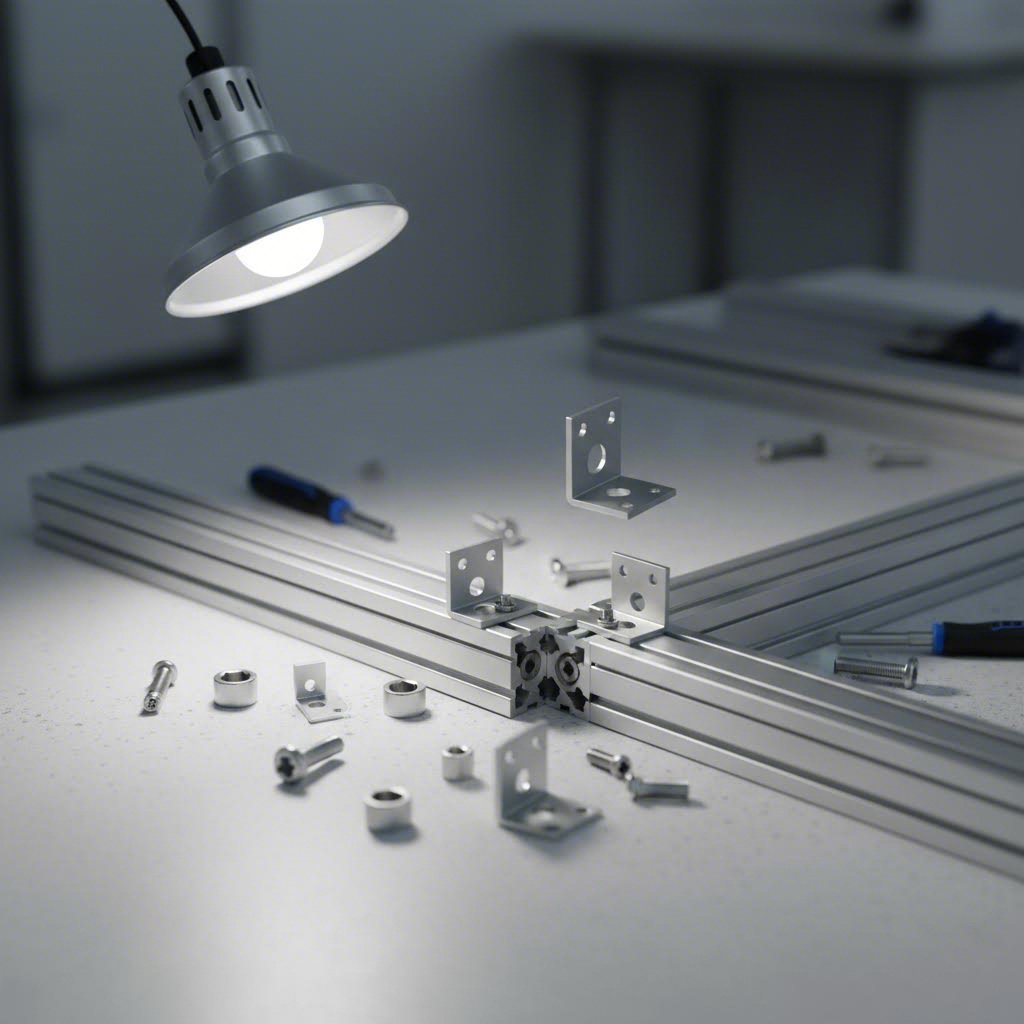
You've sourced the perfect profiles—now comes the moment of truth. How you connect those t slotted aluminum members determines whether your structure performs as engineered or becomes a wobbly disappointment. The difference between a rock-solid machine frame and one that loosens under vibration often comes down to fastener selection and installation technique. Let's break down the connection options that transform individual profiles into integrated structural assemblies.
The genius of extruded t slot systems lies in their continuous mounting channels. Rather than drilling holes at fixed locations, you slide fasteners anywhere along the t slotted rail and lock them in position. This flexibility comes from a family of specialized hardware designed specifically for aluminum t channel profiles.
According to Anglelock's T-slot hardware guide, the foundation of every T-slot connection starts with the humble T-nut. These fasteners feature a head shaped to slide into the profile's channel, with threaded holes accepting bolts from attached components. But not all T-nuts serve the same purpose:
Installing drop-in nuts takes practice. You'll rotate the nut 90 degrees to slip it into the aluminum t track slot, then rotate it back to engage the channel walls before tightening. It sounds simple, but fumbling with tiny hardware inside partially assembled frames tests patience—spring-loaded versions justify their premium in labor savings alone.
Beyond basic T-nuts, connection methods span a spectrum from simple brackets to sophisticated self-aligning systems. Choosing appropriately requires matching connection strength to application demands.
Light-duty connections (displays, shelving, cable management):
Standard structural joints (workstations, enclosures, machine guards):
High-load applications (machine bases, heavy equipment, vibration-prone assemblies):
As GAP Engineering explains, the through-connection method creates exceptionally strong joints by drilling access holes and threading directly into the mating profile. While requiring additional machining, this approach excels in demanding applications exposed to shock loading and vibration.
Here's what catalog shopping won't teach you: proprietary fastening systems like Power-Lock and similar self-aligning mechanisms represent a fundamentally different approach to t rail extrusion assembly. Rather than relying on friction from tightened bolts, these systems use mechanical interlocking that maintains joint integrity even if fasteners loosen slightly.
Self-aligning framing systems offer distinct advantages over traditional T-slot connections:
Traditional corner brackets—whether die-cast aluminum or extruded aluminum versions—remain the workhorse for most applications. Die-cast brackets include locating tabs for easier alignment but may struggle with rotational loads when used alone. Extruded brackets offer superior aesthetics and come in 45-degree configurations, though they require more careful positioning during installation.
For structures facing significant movement or vibration, combining multiple connection methods maximizes structural integrity. A machine frame might use through-connections at primary structural joints, reinforced brackets at secondary connections, and articulated joints for adjustable bracing—each component selected for its specific role in the overall structure.
Proper fastener selection means nothing if connections are spaced poorly. For distributed loads—like panel mounting or linear force applications—connection patterns must ensure adequate strength at reasonable cost.
Follow these spacing guidelines:
Remember that bolt size doesn't always equal strength. As industry experts note, an M6 bolt with 12.9 strength rating can match an M8 bolt rated at 10.9. Focus on connection engineering rather than simply upsizing hardware—proper joint design outperforms brute-force oversizing every time.
With assembly methods and fastening systems understood, you're equipped to transform your carefully selected profiles into functional structures. The final step? Establishing a systematic approach to sourcing these components and selecting manufacturing partners who can support your project from initial specification through successful implementation.
You've absorbed a tremendous amount of technical knowledge—alloy grades, temper codes, profile series, surface treatments, and assembly methods. But here's where that knowledge transforms into action. Sourcing structural aluminum extrusions successfully requires synthesizing everything you've learned into a systematic decision framework, then identifying manufacturing partners capable of delivering exactly what your project demands. Let's convert education into execution.
Before contacting any supplier or browsing where to buy aluminum extrusion options, document your requirements systematically. Rushed specifications lead to mismatched components, costly revisions, and project delays. This framework ensures you've considered every critical factor:
Working through these steps before engaging suppliers positions you to communicate requirements clearly, evaluate quotes accurately, and avoid mid-project specification changes that inflate costs.
Not all extrusion profiles suppliers are created equal. The difference between a transactional vendor and a true manufacturing partner becomes apparent when your project encounters complexity—custom requirements, tight tolerances, or demanding timelines.
When evaluating potential suppliers, assess these capabilities:
Shengxin Aluminium's deep processing services exemplify the comprehensive capability profile that simplifies complex projects. With 35 extrusion presses, state-of-the-art CNC machining centers, and complete surface treatment facilities including custom anodizing colors, powder coating, and PVDF application, they provide end-to-end solutions from die development through finished components—eliminating the multi-vendor coordination that often derails project timelines.
Transforming your documented requirements into delivered components follows a predictable path when you're working with capable partners:
The value of working with experienced, fully-equipped manufacturing partners extends beyond transaction efficiency. When questions arise during assembly, when field modifications become necessary, or when your next project builds on lessons learned, established supplier relationships provide continuity and accumulated understanding of your specific requirements.
Profile precision extrusions meeting demanding specifications don't happen by accident—they result from clear communication, appropriate material selection, capable manufacturing, and quality-focused execution throughout the supply chain. By applying the framework developed throughout this guide, you're positioned to source structural aluminum extrusion profiles that perform exactly as your application demands, assembled into structures that serve reliably for years to come.
Aluminum extrusion is a manufacturing process where heated aluminum billets (750-900°F) are forced through precision steel dies under hydraulic pressure up to 15,000 tons. The aluminum emerges with a consistent cross-sectional shape matching the die design. This process creates everything from simple solid bars to complex hollow profiles with multiple internal voids, delivering remarkable dimensional consistency that machining cannot match economically.
T-slot series numbers indicate the profile's base dimension. For metric series, the number directly represents millimeters—a 40 series profile measures 40mm x 40mm. For fractional (imperial) series, multiply by ten for inches. Larger series handle greater loads with wider slots accepting heavier-duty fasteners. Common options include 20 series for lightweight applications, 40 series for industrial frames, and 80 series for maximum load capacity and long spans.
6063-T5 offers excellent extrudability for complex thin-walled profiles with superior surface finish, making it ideal for architectural and modular framing applications with yield strength around 21,000 PSI. 6061-T6 provides higher strength (40,000 PSI yield) and excellent machinability, best for demanding structural applications and extensive secondary machining. Choose 6063 for intricate shapes and anodized finishes; select 6061 when maximum strength and machining are priorities.
T-slotted profiles excel when reconfigurability matters—workstations, machine guards, and enclosures benefit from bolt-together assembly requiring no welding. Traditional shapes (angles, channels, tubes) offer higher load capacity at lower material cost with established engineering data, ideal for permanent welded structures. Many projects combine both: T-slot for adjustable elements mounted to welded bases for maximum rigidity.
Evaluate suppliers based on manufacturing capability (own extrusion presses vs. reselling), press range for various profile sizes, in-house deep processing services (CNC machining, cutting, drilling), surface treatment options, and ISO quality certifications. Partners like Shengxin Aluminium offer comprehensive solutions with 35 extrusion presses, advanced CNC centers, and complete finishing capabilities—eliminating multi-vendor coordination while ensuring consistent quality from die development through delivered components.


 บริการออนไลน์
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 ไทย
 English
 français
 Deutsch
 русский
 español
 português
 العربية
 Việt
 Українська