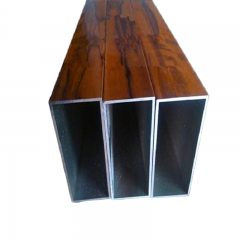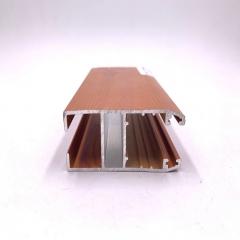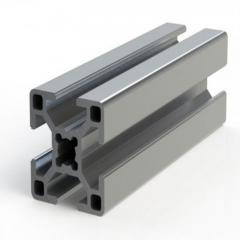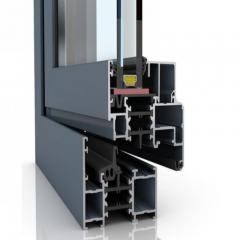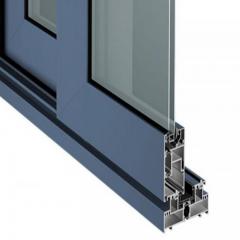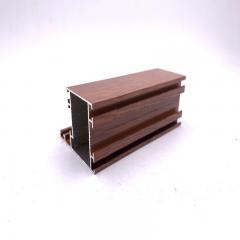
When you look at the sleek window frames on a modern building or the durable trim on industrial equipment, you're likely seeing painted aluminum extrusions at work. But what exactly goes into transforming raw extruded aluminum into these finished, high-performance components?
Painting services for aluminum extrusions encompass the specialized processes used to apply protective and decorative coatings to extruded aluminum profiles. Unlike painting wood or steel, aluminum painting requires unique preparation methods and coating systems designed specifically for this metal's surface characteristics.
Raw aluminum extrusions come directly from the press with a mill finish—a natural, uncoated surface that offers only minimal protection. While aluminum does form a thin natural oxide layer that provides some corrosion resistance, this layer simply isn't enough for most real-world applications. Professional finishing services bridge this gap by applying engineered coating systems that dramatically enhance both performance and appearance.
According to the Aluminum Extruders Council, aluminum extrusions are rarely utilized as they come from the press and commonly undergo secondary finishing operations to transform them into functional components for their intended applications.
Imagine installing untreated aluminum profiles on a coastal building. Within months, you'd notice pitting, discoloration, and degraded performance. Proper aluminum painting prevents these issues while opening up endless design possibilities.
Professional coating services deliver several critical benefits:
The key to successful aluminum painting lies in understanding that this metal requires specialized preparation. Surface treatments like chemical conversion coatings create the foundation for proper paint adhesion—skip this step, and even premium coatings will fail prematurely. Whether you're specifying finishes for architectural facades, automotive components, or industrial equipment, selecting the right coating system matched to your application's demands is essential for long-term performance.
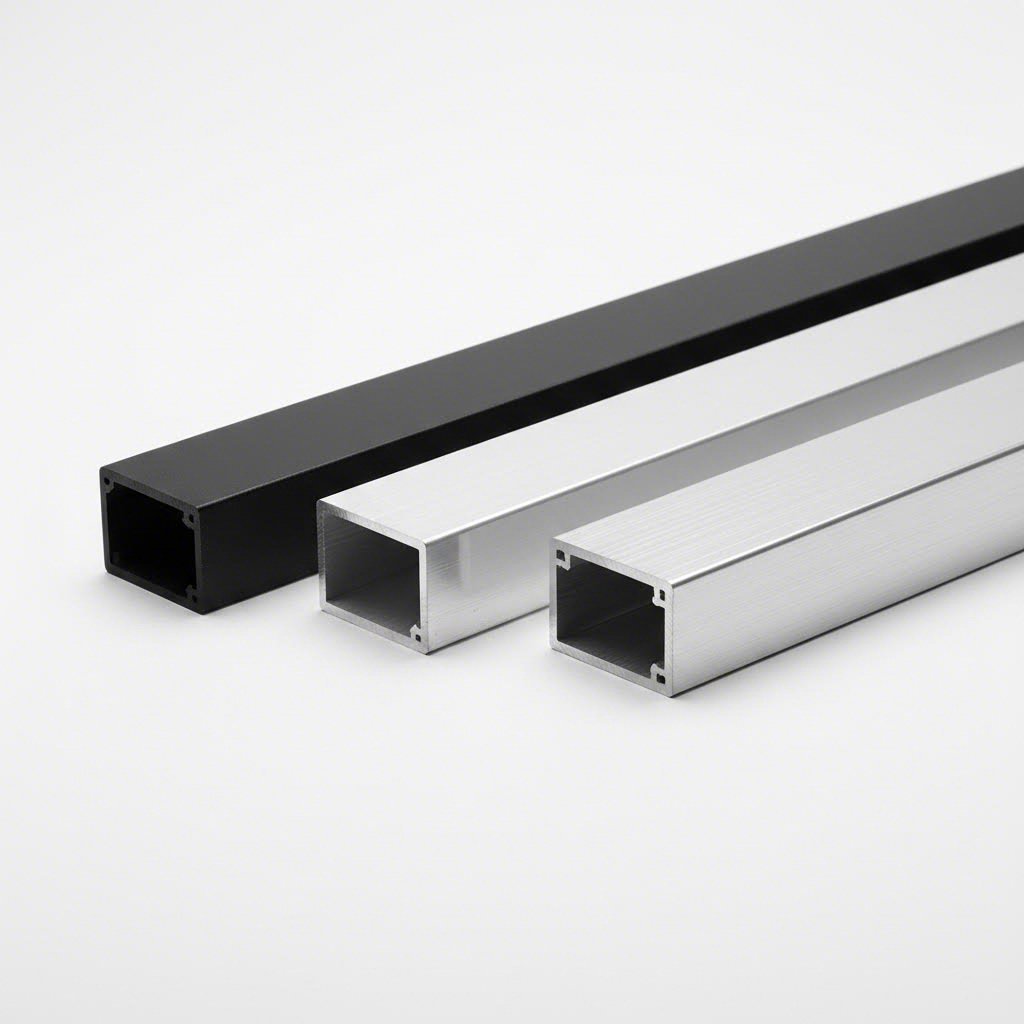
Now that you understand why surface finishing matters, the next question is straightforward: which finishing method should you choose? Three primary options dominate the aluminum extrusion market—liquid painting, powder coating, and anodizing. Each brings distinct advantages depending on your project's performance requirements, aesthetic goals, and budget constraints.
When comparing powder coating to traditional liquid paint, think of it as choosing between two fundamentally different application philosophies. Liquid paint uses solvents to keep pigments suspended until application, while powder coating applies dry powder electrostatically and cures it with heat—no solvents required.
Powder coating has become the preferred choice for many outdoor aluminum applications. According to industry experts, the cured powder finish is much thicker than liquid paint, providing enhanced resistance to chipping, scratching, fading, and general wear. This durability advantage makes powder coating ideal for architectural components, outdoor furniture, and industrial equipment exposed to harsh conditions.
However, liquid paint maintains important advantages in specific scenarios:
One common concern with powder coating is the orange peel effect—a textured surface appearance resembling the skin of an orange. This defect occurs when application parameters like powder particle size, spray gun settings, or curing temperatures aren't properly controlled. Experienced applicators prevent this issue through proper technique and equipment calibration, but it remains a consideration when evaluating potential service providers.
Anodized aluminum extrusions represent something entirely different from painted or powder-coated surfaces. Rather than applying a coating on top of the metal, anodizing creates an integral oxide layer that grows from the aluminum itself through an electrochemical process.
This distinction matters significantly for durability. As noted by SAF, the anodic coating is integral to the metal and cannot peel or flake. Aluminum oxide is exceptionally hard and weather-resistant, providing superior abrasion resistance compared to organic coatings. This makes anodized extruded aluminum the preferred choice for high-traffic areas like door frames, kick plates, and handrails where physical wear is a primary concern.
Anodizing offers another unique advantage: renewability. When an anodized surface accumulates dirt or appears to have degraded, cleaning with mild detergent and gentle abrasion can actually remove a small amount of the oxide layer, revealing a renewed finish beneath. Painted surfaces, once they fail, require complete recoating—a far more expensive proposition.
However, anodized aluminum extrusion finishes have limitations. Color options are more restricted than with paint systems, typically limited to clear, bronze tones, and certain dyed colors. The process also struggles with chemical resistance in highly acidic urban environments, where pollutants can eventually compromise the oxide layer.
| Factor | Liquid Paint | Powder Coating | Anodizing |
|---|---|---|---|
| Durability | Moderate; prone to chipping and scratching | Excellent; thick, resilient finish resists wear | Superior abrasion resistance; integral to metal |
| Color Options | Unlimited; easy custom matching | Wide variety; custom colors require larger batches | Limited to clear, bronze, black, and select dyed colors |
| Typical Cost | Lower setup; higher per-unit for small runs | $0.12–$0.35/cm²; economical for large batches | $0.10–$0.30/cm²; varies by thickness class |
| Environmental Impact | VOC emissions from solvents; waste from overspray | Near-zero VOCs; overspray reclaimed and reused | No VOCs; byproducts often beneficial for wastewater treatment |
| Ideal Applications | Detail work, small batches, custom colors, heat-sensitive substrates | Outdoor architectural, automotive, industrial equipment | Storefronts, handrails, high-traffic areas, metallic appearance |
| Coating Thickness | Thin, precise control possible | 60–120 μm typical; thicker than liquid | Class I (0.7 mil) or Class II (0.4 mil) per AA standards |
| Repairability | Touch-up possible but visible | Difficult to repair; often requires full recoat | Renewable through cleaning; surface can be restored |
So which method should you specify? The answer depends on your project's specific demands:
Many projects actually combine methods—anodized door components with powder-coated curtainwall framing, for example. Understanding these distinctions positions you to specify the right finish for each component based on its unique performance requirements rather than applying a one-size-fits-all approach.
With the finishing method selected, the next critical decision involves understanding the performance standards that govern coating quality—particularly the AAMA specifications that define what constitutes acceptable performance for architectural applications.
You've selected your finishing method—now comes an equally important decision. How do you ensure the coating actually performs as expected for years or even decades? This is where AAMA standards enter the picture, providing the benchmark specifications that separate premium extrusion finish quality from coatings that fail prematurely.
The American Architectural Manufacturers Association (now known as FGIA—Fenestration and Glazing Industry Alliance) developed these standards to define and verify coating durability for architectural applications. According to AAMA guidelines, these specifications outline the performance requirements for organic coatings on architectural aluminum extrusions and panels, ensuring products can withstand environmental challenges including wind, rain, sun, and corrosive conditions.
Think of these three specifications as performance tiers—each designed for increasingly demanding applications. Understanding their differences helps you specify the right protection level without over-engineering (and overspending) or under-specifying (and risking premature failure).
AAMA 2603: Basic Protection
This entry-level specification suits interior applications and sheltered exterior uses where environmental exposure is minimal. AAMA 2603 powder and liquid coatings undergo just one year of outdoor weathering exposure testing in South Florida—the industry's standard harsh-weather testing location. While these coatings must meet basic gloss requirements (within +/- 5 units of manufacturer specifications), the standard sets no specific thresholds for gloss retention or erosion resistance after weathering.
When is AAMA 2603 appropriate? Consider interior aluminum trim, office partition framing, or exterior components protected by overhangs where direct weather exposure is limited. The lower testing requirements translate to cost savings—but only when the application truly doesn't demand more.
AAMA 2604: Moderate Durability
Commonly called "Super Durable," AAMA 2604 represents a significant step up for exterior applications. Coatings meeting this standard endure five years of South Florida weathering exposure and must demonstrate measurable performance retention:
AAMA 2604 works well for ground-level applications or components within reach of building occupants. The coating system's enhanced durability handles physical contact and handling better than 2605-rated finishes, making it practical for entryways, storefronts, and accessible facade elements.
AAMA 2605: Premium Performance
For the most demanding exterior applications, AAMA 2605 sets the gold standard. These high-performance coatings—typically fluoropolymer-based systems like PVDF (Kynar)—undergo a full decade of weathering exposure testing with stringent requirements:
When you're specifying coatings for high-rise curtainwall systems, exposed building facades, or any architectural component where maintenance access is difficult and appearance is critical, AAMA 2605 delivers the long-term performance that protects your investment.
Selecting the appropriate AAMA standard isn't simply about choosing the "best"—it's about matching performance requirements to your specific application. Specifying AAMA 2605 for interior applications wastes budget on unnecessary performance, while choosing AAMA 2603 for exposed coastal installations sets up your project for premature coating failure.
Consider these decision factors:
For product on building facades or out of reach, architects and building owners can be confident that structures coated to AAMA 2604 or AAMA 2605 will maintain their beauty and performance for decades, reducing maintenance needs and minimizing lifecycle costs.
When communicating with painting service providers, always specify the AAMA standard explicitly in your documentation. This simple step ensures everyone understands the performance expectations and testing requirements your project demands—protecting both aesthetic intent and long-term coating durability.
Of course, even the best specification means nothing without proper execution. Understanding the complete painting process—from surface preparation through final curing—reveals why process quality matters just as much as the coating specification itself.
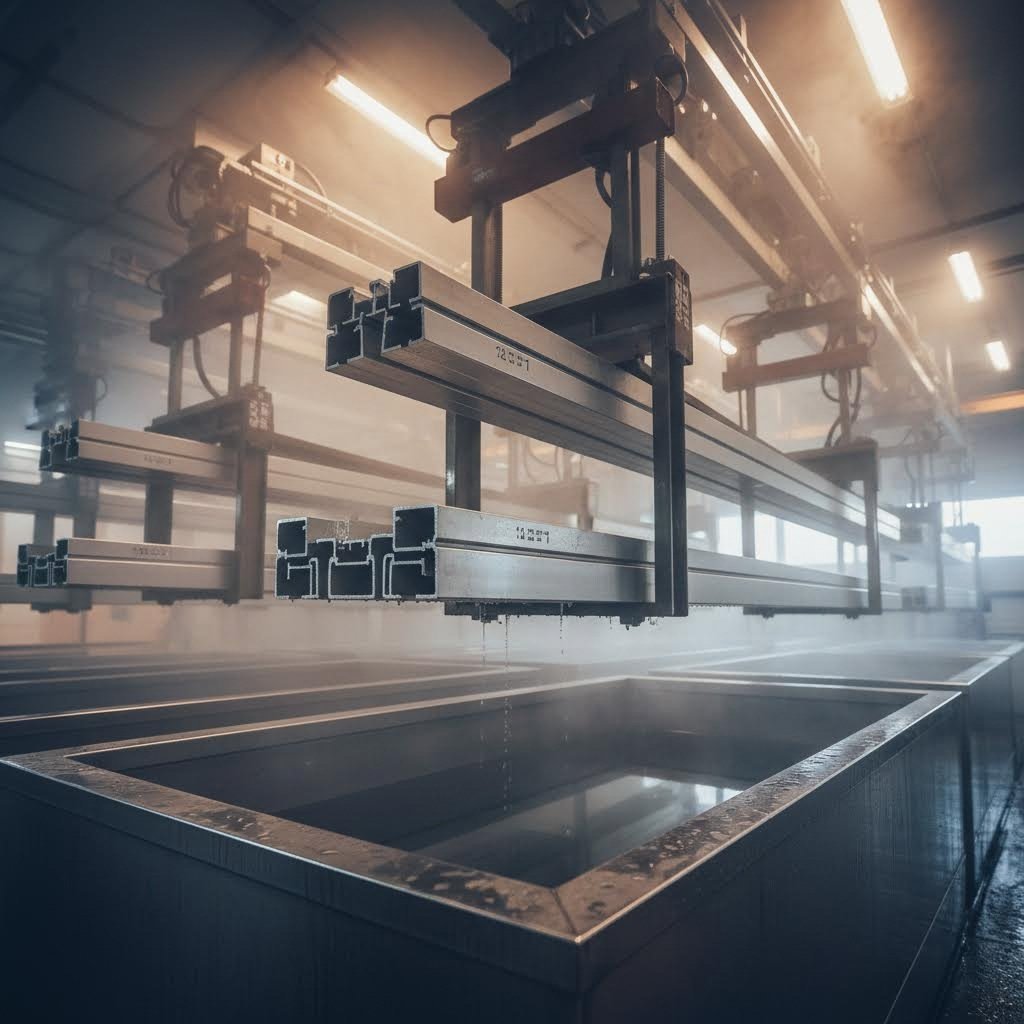
So how do you paint aluminum extrusions the right way? Whether you're managing a large architectural project or sourcing components for industrial equipment, understanding the complete finishing process helps you evaluate service providers, troubleshoot quality issues, and ensure your specifications translate into durable, long-lasting results.
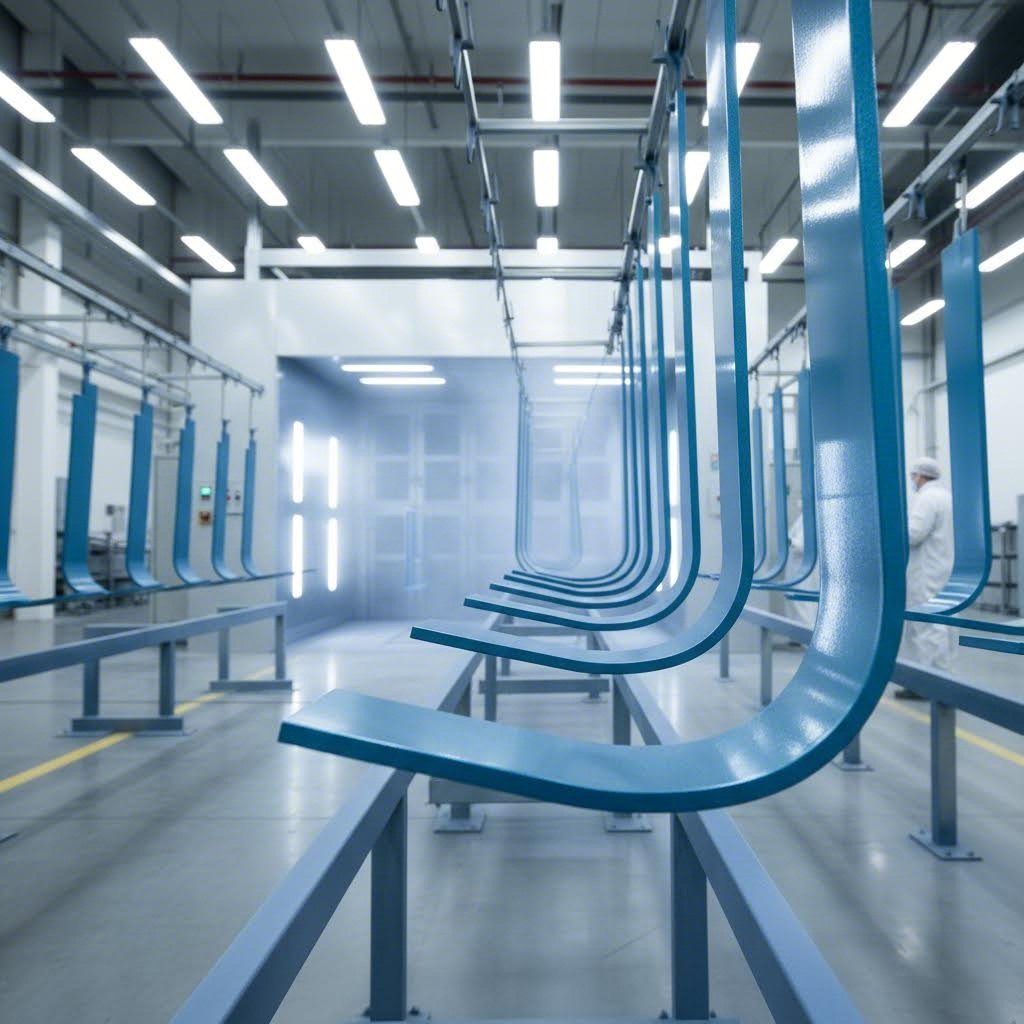
The truth is, painting aluminum isn't as simple as applying color to metal. Skip any critical step, and even premium coatings will fail—sometimes within months. Let's walk through each stage so you'll know exactly what separates professional-quality aluminium painted finishes from shortcuts that lead to adhesion failures and warranty claims.
Here's something many people don't realize: surface preparation typically determines 80% of a coating's long-term performance. Aluminum's natural oxide layer and smooth surface create adhesion challenges that require systematic treatment before any coating is applied.
The complete pre-treatment sequence follows a specific order, with each step building on the previous one:
Why does this sequence matter so much? Imagine applying paint over an invisible film of oil or onto a surface with inconsistent conversion coating coverage. The paint might look perfect initially, but within weeks or months, you'll see peeling, blistering, or adhesion loss—particularly in areas exposed to moisture or temperature cycling.
Professional finishing operations maintain strict process controls at each stage: chemical concentrations, temperature ranges, immersion times, and rinse water quality. When evaluating painting service providers, asking about their pre-treatment process quality controls reveals much about their commitment to durable results.
With properly prepared surfaces, application can begin. The method chosen depends on the coating type, production volume, and finish quality requirements.
Common Application Methods
Preventing the Orange Peel Effect
You'll recall we mentioned the orange peel texture issue earlier—that unwanted surface texture that resembles citrus skin. In powder coating applications, this defect typically results from improper settings or process conditions:
Experienced applicators prevent orange peel by controlling these variables and conducting regular quality checks. When evaluating aluminium painted sample panels from potential suppliers, surface smoothness provides a quick indicator of their process control quality.
Curing Requirements
Proper curing transforms applied coatings into their final hardened state. This step is non-negotiable—under-cured coatings remain soft and vulnerable, while over-curing can cause brittleness and color shifts.
Typical curing parameters vary by coating type:
Quality finishing operations use calibrated ovens and temperature monitoring systems to document that every batch achieves required cure specifications. This documentation becomes especially important when coatings must meet AAMA standards requiring specific performance characteristics.
Understanding this complete process—from initial cleaning through final cure—positions you to ask the right questions when sourcing finishing services. It also explains why cutting corners at any stage inevitably leads to premature coating failures that cost far more than doing it right the first time.
Of course, the process alone doesn't tell the whole story. The aluminum alloy itself significantly influences how well coatings adhere and perform—a factor many specifiers overlook when planning their finishing requirements.
Here's something that often catches specifiers off guard: not all aluminum extrusions paint the same way. The alloy you choose for structural performance, corrosion resistance, or extrudability directly affects how well coatings adhere and how the finished surface appears. Understanding these relationships helps you avoid unexpected finishing problems—and ensures your painting service provider has the information they need to deliver optimal results.
Aluminum alloys aren't pure aluminum. They contain carefully balanced additions of elements like magnesium, silicon, copper, and zinc that modify the metal's properties. These alloying elements also influence surface characteristics that matter during finishing.
Think about it this way: the conversion coating process creates a chemical bond with the aluminum surface. When that surface contains different elements at varying concentrations, the chemical reactions behave differently—sometimes subtly, sometimes significantly.
Several factors come into play:
The practical result? An aluminum colored paint finish that looks flawless on one alloy might show adhesion problems, surface texture variations, or color inconsistencies on another—even when the same coating system and application process are used.
Let's examine the alloys you're most likely to encounter and their finishing considerations.
6063 Aluminum: The Finishing-Friendly Standard
If you're working with architectural or decorative aluminum extrusions, chances are you're dealing with 6063 alloy. This magnesium-silicon alloy dominates the extrusion market for good reason—it offers excellent extrudability, good corrosion resistance, and outstanding surface finish characteristics.
From a painting perspective, 6063 is about as cooperative as aluminum gets. Its moderate alloying element content produces consistent, uniform surfaces that respond predictably to standard pre-treatment processes. Conversion coatings form evenly, and adhesion is rarely problematic when proper procedures are . This alloy represents the baseline against which other alloys are often compared for paintability.
6061 Aluminum: Structural Versatility
When you need higher strength than 6063 provides, 6061 is often the next choice. This alloy contains slightly more magnesium and adds copper and chromium to the mix. While still very paintable, 6061 may show slightly more variability in surface response during chemical pre-treatment. Standard finishing procedures work well, but quality control becomes somewhat more important to ensure consistent results across production runs.
7075 Aluminum: High-Strength Challenges
For demanding structural applications—think extruded aluminum strut systems in aerospace or high-performance equipment—7075 and similar 7xxx-series alloys provide exceptional strength-to-weight ratios. However, their high zinc and copper content creates finishing complications.
These alloys often require modified pre-treatment procedures:
Finishing 7075 successfully isn't impossible—it simply demands expertise and process modifications that not every painting service provider offers.
Aluminum Struts and Structural Profiles
Here's where alloy selection intersects with application requirements. Aluminum struts used in framing systems, industrial equipment, or structural support often prioritize strength and load-bearing capacity over surface finish quality. These components may use 6061, 6082, or even 7xxx-series alloys depending on performance requirements.
The coating requirements for structural aluminum struts also differ from architectural components:
| Alloy | Primary Uses | Paintability | Key Considerations |
|---|---|---|---|
| 6063 | Architectural, decorative, window frames | Excellent | Industry standard for finishing; responds well to standard pre-treatment |
| 6061 | Structural components, marine, automotive | Very Good | Slightly higher variability; may need tighter process control |
| 6082 | Structural applications, bridges, cranes | Good | Higher silicon content may affect surface uniformity |
| 7075 | Aerospace, high-stress structural, extruded aluminum strut | Moderate | Requires modified pre-treatment; specialist expertise recommended |
| 5052 | Marine, chemical equipment, tanks | Good | High magnesium content may require adjusted etch parameters |
Communicating Alloy Specifications to Your Provider
When sourcing painting services for aluminum extrusions, don't assume your provider knows what alloy they're finishing. Always communicate this information explicitly—it directly affects the pre-treatment approach and quality expectations.
Include these details in your specifications:
This information enables your finishing provider to adjust their process accordingly—or to flag potential concerns before production begins. A provider who asks about alloy specifications demonstrates finishing expertise; one who doesn't may lack the technical depth to handle challenging alloys successfully.
With alloy considerations addressed, the next question becomes: what happens when coatings don't perform as expected? Understanding common painting failures—and how to prevent them—protects your investment and helps you evaluate coating quality before problems become expensive.
Even when you specify the right AAMA standard and select an appropriate alloy, coating failures can still occur. Understanding why painted aluminium fails—and how to prevent these problems—saves you from costly rework, project delays, and warranty disputes. Let's examine the most common defects and the prevention strategies that ensure your aluminium paints deliver lasting performance.
Coating failures rarely happen randomly. Each defect type traces back to specific root causes, and recognizing these patterns helps you identify problems early—or prevent them entirely.
Adhesion Failure
When paint for cast aluminium or extruded profiles peels, flakes, or lifts from the surface, you're witnessing adhesion failure. This represents the most serious coating defect because it completely compromises protection. Common causes include:
Chalking and Fading
Over time, some coatings develop a powdery surface residue (chalking) or lose their original color intensity (fading). While some degradation is normal over decades of exposure, premature chalking or fading indicates problems:
Blistering
Bubbles or raised areas in the coating surface signal moisture trapped beneath the paint film. This defect typically originates from:
Cracking and Checking
Fine cracks or a pattern resembling dried mud indicate coating brittleness—often from over-curing, excessive film thickness, or coating systems that lack flexibility for thermal expansion cycles.
Preventing coating failures starts with understanding that quality happens at every process stage—not just during final inspection. Here's how to protect your investment.
Environmental Control During Application
Application conditions dramatically affect finish quality. Professional finishing facilities control these variables rigorously:
Quality Verification Procedures
Don't wait for installation to discover coating problems. Effective quality verification catches issues while correction is still practical:
Always request test reports and quality documentation from your finishing provider. Reputable operations maintain records of film thickness, adhesion testing, and cure verification for every production batch.
Proper Storage and Handling
Painted aluminium can be damaged before it ever reaches the job site. Protect your investment with proper handling practices:
Warning Signs to Watch For
When evaluating painted extrusions—whether incoming materials or installed components—watch for these red flags that indicate potential problems:
Catching these issues early—ideally during incoming inspection before installation—prevents costly removal and refinishing of installed materials. When you understand what quality looks like and how to verify it, you're positioned to hold finishing providers accountable and protect your project outcomes.
With quality assurance fundamentals covered, the next consideration involves the aesthetic possibilities available—the colors, textures, and specialty finishes that transform functional aluminum into design elements.
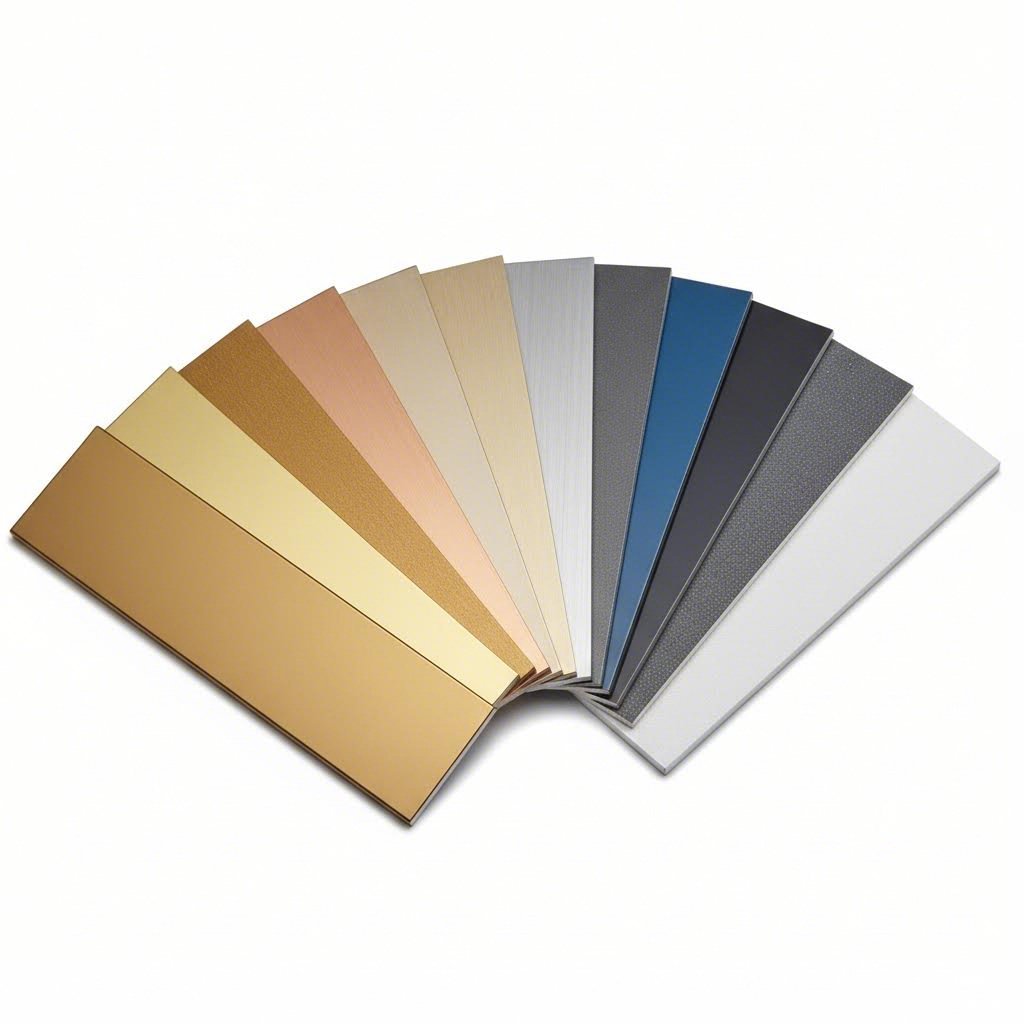
You've addressed the technical requirements—AAMA standards, alloy compatibility, and quality assurance procedures. Now comes the question that often drives the final specification: what color and finish will bring your design vision to life? The range of options available for aluminum extrusions extends far beyond basic whites and bronzes, offering possibilities that can match virtually any architectural or industrial aesthetic.
When specifying colors for painted aluminum extrusions, you'll encounter two primary paths: standard color selections and custom color matching. Understanding the differences helps you balance design requirements against budget and timeline constraints.
Standard RAL and Manufacturer Colors
The RAL color system—developed in Germany and now used worldwide—provides a standardized palette of over 2,500 colors that finishing providers keep readily available. Specifying a RAL number (like RAL 7016 Anthracite Grey or RAL 9010 Pure White) ensures consistency across suppliers and production runs.
Most powder coating and liquid paint manufacturers also maintain their own standard color libraries. These pre-formulated colors offer several advantages:
Custom Color Matching Services
When standard colors won't satisfy your project requirements, custom color matching creates exact formulations to match specific samples. You might need to match existing building components, corporate brand colors, or unique design specifications.
The matching process typically works like this: you provide a physical sample—whether a painted chip, fabric swatch, or even an anodized color sample from a previous project—and the coating formulator develops a recipe that replicates it within specified tolerances. Using anodized color samples as reference can be particularly helpful when projects require finishes that coordinate with existing anodized components while offering the broader durability options of painted coatings.
Keep in mind that custom colors require lead time for formulation, approval, and production. While standard colors might ship within days, custom matches often require two to four weeks from sample submission to first production—longer for complex metallics or specialty effects.
Color is only half the equation. The finish texture and sheen level profoundly affect how that color appears on your finished extrusions.
Gloss Levels
Finish sheen is measured in gloss units (GU) at specific angles, typically 60 degrees. Common classifications include:
Architectural specifications often favor satin or matte finishes because they're more forgiving of substrate variations and reduce visual distractions from reflected light. Industrial applications may prioritize cleanability, making semi-gloss finishes practical choices.
Textured Finishes
Beyond smooth coatings, textured powder coatings add visual and tactile dimension to aluminum surfaces. Options range from subtle sand textures to aggressive hammertone patterns. Textured finishes offer practical benefits:
Specialty and Decorative Finishes
Advanced coating technologies have expanded finish possibilities dramatically. According to ForMe Design, modern aluminum finishing now includes four premium finish categories: Powder on Powder, Sublimation, HD printing, and standard Powder Coating—each capable of reproducing wood grain, metal, and stone effects with remarkable realism.
These specialty finishes enable aluminum extrusions to mimic natural materials while retaining aluminum's performance advantages:
Finish Categories by Application
Matching finish selection to application requirements simplifies decision-making:
Color Consistency and Tolerance Specifications
Production realities mean that color matching is never perfect—acceptable variation must be defined. Color tolerance is measured using Delta E values, which quantify the perceivable difference between two colors:
When specifying custom colors, explicitly state your acceptable Delta E tolerance. Also consider batch-to-batch variation—if your project receives materials from multiple production runs, tighter tolerances prevent visible color shifts across installed components.
With the aesthetic possibilities now clear, the practical question becomes: how do you find a finishing provider capable of delivering these options reliably and cost-effectively?
You've defined your AAMA requirements, selected your colors, and understand what quality looks like. Now comes a decision that determines whether those specifications translate into actual results: choosing the right finishing partner. Whether you're sourcing a single prototype run or planning ongoing production, the provider you select shapes your project's timeline, quality outcomes, and total cost.
Not all coating service providers offer the same capabilities—or deliver the same consistency. Let's walk through the evaluation process so you can identify partners who'll meet your requirements reliably.
When you're vetting potential finishing providers, the right questions reveal capabilities that marketing materials often obscure. Before requesting quotes, gather answers to these essentials:
A complete Request for Quotation prevents misunderstandings and enables accurate pricing. Include these elements:
The more complete your RFQ, the more accurate the quotes you'll receive—and the fewer surprises you'll encounter during production.
Should you handle finishing internally or partner with a specialized coating service? This strategic decision affects more than just cost—it shapes your quality control, flexibility, and project timelines.
For most organizations, outsourcing to specialized coating services makes practical sense. According to GlobalSpec, coating services are used by companies that do not have coating technology and equipment in house—and once a part is ready for coating, the manufacturer contacts the coating shop with material and process specifications for minimal turnaround time.
The key is finding providers whose capabilities match your requirements. Location matters too—transporting aluminum extrusions adds cost and time, so regional providers often offer advantages for routine production while national specialists may be worth the logistics for complex or high-specification work.
Here's where the decision gets interesting. Some manufacturers offer both extrusion and finishing under one roof—eliminating the coordination challenges of working with separate suppliers.
Consider what happens with fragmented supply chains: you order extrusions from one company, ship them to a finishing provider, coordinate timing between two production schedules, and manage quality issues across organizational boundaries. Each handoff introduces delay, handling risk, and potential miscommunication.
Integrated service providers streamline this entirely. Facilities with comprehensive capabilities—such as those offering anodizing in custom colors, powder coating, PVDF, and micro-arc oxidation—provide flexibility for diverse project requirements without multiplying your vendor relationships. When the same organization controls die development, extrusion, and surface treatment, accountability is clear and communication is direct.
This integration becomes especially valuable for complex projects requiring multiple finish types. You might need anodized components for high-traffic areas, powder-coated profiles for general facade work, and PVDF finishes for critical exposed elements—all coordinated from a single source.
Experienced providers with advanced surface treatment options can support projects from die development through finished coating, offering end-to-end support that simplifies project execution. For readers seeking this type of integrated extrusion and finishing solution, Shengxin Aluminium's processing services demonstrate how comprehensive manufacturing and finishing capabilities can work together—with 35 extrusion presses, CNC machining centers, and diverse surface treatment options including anodizing, powder coating, and PVDF all available from a single facility.
Beyond certifications and equipment lists, how do you assess whether a provider will actually deliver quality results? These practical evaluation steps help:
The finishing provider you select becomes a long-term partner affecting every project's success. Investing time in thorough evaluation upfront prevents quality problems, missed deadlines, and costly supplier changes later—setting the foundation for reliable, high-quality painted aluminum extrusions that meet your specifications consistently.
With your provider selected, one final consideration increasingly shapes finishing decisions: environmental impact and sustainability requirements that are transforming coating technology choices.
Sustainability isn't just a buzzword anymore—it's reshaping how aluminum extrusions are finished. From tightening regulations on hazardous chemicals to growing customer demand for greener supply chains, environmental considerations now influence coating decisions as much as performance specifications do.
The good news? Modern eco-friendly aluminum coating technologies often deliver equal or superior performance while reducing environmental impact. Understanding these options positions you to make finishing decisions that satisfy both regulatory requirements and sustainability goals.
The aluminum finishing industry has undergone significant transformation in recent years. Two developments stand out: the shift away from chromium-based pretreatments and the adoption of low VOC aluminum paint formulations.
Chrome-Free Pretreatment Systems
Remember the conversion coating step we discussed in the painting process? Traditionally, chromate conversion coatings containing hexavalent chromium provided excellent corrosion protection and paint adhesion. However, hexavalent chromium is a known carcinogen—and regulations are eliminating it from manufacturing processes worldwide.
According to FP360 Group, trivalent chromium (Cr+3) conversion coatings offer much lower toxicity than hexavalent chromium while delivering corrosion resistance competitive with legacy systems. For many alloy systems, these coatings mitigate regulatory risk without sacrificing performance.
Chrome-free pretreatment alternatives go even further, eliminating chromium entirely:
Specifying chrome-free pretreatment future-proofs your projects against tightening regulations while reducing hazardous waste disposal costs and worker exposure risks.
Low-VOC and Zero-VOC Coating Systems
Volatile organic compounds (VOCs) in traditional liquid paints contribute to air pollution and create health hazards for workers. Sustainable powder coating addresses this concern directly—powder coatings emit near-zero VOCs during application because they contain no solvents.
But the environmental advantages of powder coating extend beyond VOC elimination:
For applications requiring liquid coatings, water-based and high-solids formulations now offer performance approaching traditional solvent-based systems while dramatically reducing VOC emissions.
Environmental responsibility in aluminum finishing extends beyond chemical choices to encompass energy consumption, end-of-life considerations, and overall lifecycle impact.
Energy Efficiency in Curing Processes
Curing ovens represent significant energy consumers in coating operations. Modern finishing facilities are adopting several strategies to reduce this footprint:
Sustainable processing and treatment options like secondary smelting, eco-friendly anodizing, and chromium-free coatings offer a path to cut emissions and reduce waste while also improving cost efficiency and market competitiveness.
Recyclability and End-of-Life Considerations
Here's something remarkable about painted aluminum: it remains fully recyclable. During aluminum recycling, organic coatings simply burn off in the remelt process, leaving pure aluminum for reuse. This circular potential is extraordinary—according to the International Aluminum Institute, 75% of all aluminum ever produced is still in use today.
Powder coatings and most liquid paint systems don't contaminate the aluminum substrate in ways that prevent recycling. This means your painted extrusions can eventually return to the material stream, requiring roughly 95% less energy than producing primary aluminum from ore.
Regulatory Drivers of Innovation
Environmental regulations aren't just restricting harmful practices—they're accelerating innovation in coating technologies. The EU's REACH regulations have already phased out hexavalent chromium in many applications, pushing the industry toward safer alternatives. Similar restrictions are expanding globally.
Forward-thinking specifiers recognize that adopting sustainable finishing practices now provides competitive advantages:
When evaluating finishing providers, ask about their environmental practices. Facilities investing in chrome-free pretreatment, powder coating capabilities, and energy-efficient operations demonstrate commitment to sustainable manufacturing—and likely offer more future-proof coating solutions for your projects.
With environmental considerations addressed, let's bring together everything we've covered into a practical framework for planning your aluminum extrusion finishing project.
You've now explored the full landscape of painting services for aluminum extrusions—from AAMA standards and alloy compatibility to quality verification and environmental considerations. But how do you translate all this knowledge into action? Let's synthesize the critical decision factors and create a practical roadmap for your aluminum extrusion project planning.
Successful aluminum finishing projects start with clarity on four interconnected considerations. Getting these right upfront prevents costly changes mid-project and ensures your finished extrusions perform as expected.
Performance Requirements
Start here—everything else flows from performance needs. Ask yourself:
Your answers point directly to the appropriate AAMA specification. Remember: AAMA 2603 handles interior and sheltered uses, AAMA 2604 serves moderate exterior exposure, and AAMA 2605 delivers premium performance for demanding environments.
Aesthetic Goals
Once performance requirements are defined, aesthetic decisions become clearer:
Budget Constraints
Finishing costs vary significantly based on your choices:
Consider lifecycle costs, not just initial price. A premium coating that lasts 20 years without recoating often costs less over time than a basic finish requiring maintenance every 5-7 years.
Timeline Needs
Your extrusion painting timeline affects both cost and supplier options:
Ready to move forward? This aluminum finishing checklist guides you through the essential steps, ensuring nothing critical gets overlooked.
The coating specification guide principle: document everything explicitly. Assumptions lead to disputes—clear specifications protect both your project outcomes and your relationship with finishing providers.
Here's a practical reality: managing separate suppliers for extrusion and finishing multiplies your coordination burden. Every handoff between organizations introduces potential delays, handling damage, and communication gaps.
Partnering with experienced manufacturers offering end-to-end support—from custom extrusion through surface treatment—simplifies project execution considerably. When die development, extrusion production, and finishing happen under unified quality control, accountability is clear and problems get resolved faster.
Providers with decades of experience and diverse finishing capabilities including anodizing, powder coating, and PVDF can deliver consistent quality at factory-direct pricing. This integrated approach proves especially valuable for projects requiring multiple finish types or tight coordination between component deliveries.
For readers ready to explore this integrated approach, Shengxin Aluminium's comprehensive aluminum profile processing services demonstrate what end-to-end capability looks like in practice. With over 30 years of industry experience, 35 extrusion presses, and complete surface treatment options—including anodizing in custom colors like Champagne and Rose Gold, powder coating, PVDF, and micro-arc oxidation—they provide the technical depth and production capacity to support projects from initial die development through finished, coated profiles.
Whether you're specifying coatings for architectural facades, industrial equipment, or specialty applications, the principles remain consistent: define performance requirements clearly, specify appropriate standards explicitly, communicate alloy information completely, and partner with providers whose capabilities match your project's demands. Do this, and your painted aluminum extrusions will deliver the durability, appearance, and value your projects require.
Yes, extruded aluminum can be painted using specialized processes. However, aluminum requires unique surface preparation including cleaning, degreasing, and chemical conversion coating to ensure proper paint adhesion. Professional finishing services use powder coating, liquid paint, or PVDF systems that bond effectively with aluminum's surface characteristics. When properly prepared and coated to AAMA standards, painted aluminum extrusions deliver excellent corrosion resistance, UV protection, and long-term durability for both architectural and industrial applications.
The most common mistakes include skipping proper surface cleaning and degreasing, which leaves oils that prevent adhesion. Using the wrong primer or skipping primer entirely leads to coating failure. Applying paint in improper environmental conditions—high humidity or extreme temperatures—causes blistering and adhesion problems. Choosing incompatible coating systems or incorrect AAMA specifications for the application environment results in premature chalking and fading. Poor application technique creates defects like orange peel texture, runs, and uneven coverage.
AAMA 2603 provides basic protection for interior applications with one year of weathering exposure testing. AAMA 2604 (Super Durable) offers moderate durability for exterior use with five years of testing, requiring color retention below Delta E 5 and gloss retention above 30%. AAMA 2605 delivers premium performance for demanding exterior applications with ten years of testing, maintaining color retention below Delta E 5 and gloss retention above 50%. Each standard suits different environmental exposures and maintenance accessibility requirements.
Choose powder coating when outdoor durability, environmental benefits (near-zero VOCs), and cost-efficiency for larger production runs are priorities. Powder coating creates thicker, more resilient finishes ideal for architectural and industrial applications. Choose liquid paint when you need precise custom color matching, thinner coating profiles for tight tolerances, or flexibility for smaller batch sizes. Liquid systems excel at detail work and prototyping where immediate color formulation is needed.
Evaluate providers based on AAMA-licensed applicator status, ISO 9001 certification, and documented quality control procedures including film thickness and adhesion testing. Ask about pre-treatment systems (chrome-free options are increasingly preferred), turnaround capabilities, and minimum order requirements. Request sample panels to evaluate finish quality. Consider integrated service providers like Shengxin Aluminium that offer extrusion and finishing under one roof, eliminating coordination challenges while providing end-to-end support from die development through surface treatment.


 บริการออนไลน์
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 ไทย
 English
 français
 Deutsch
 русский
 español
 português
 العربية
 Việt
 Українська