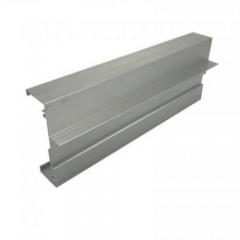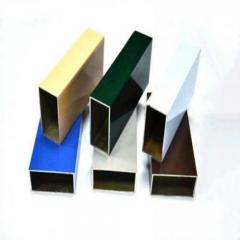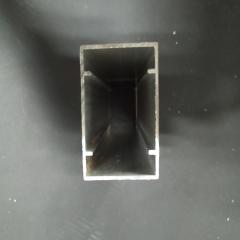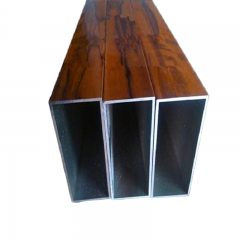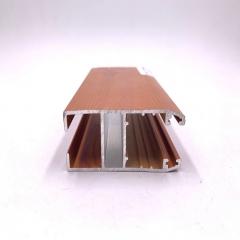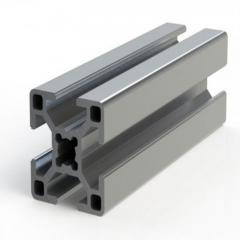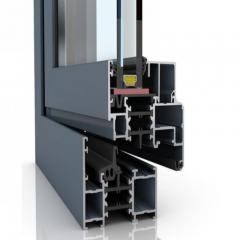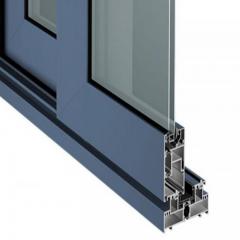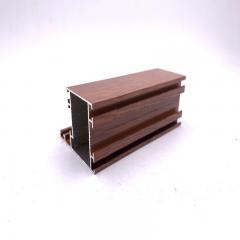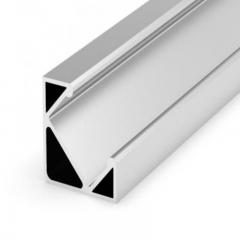
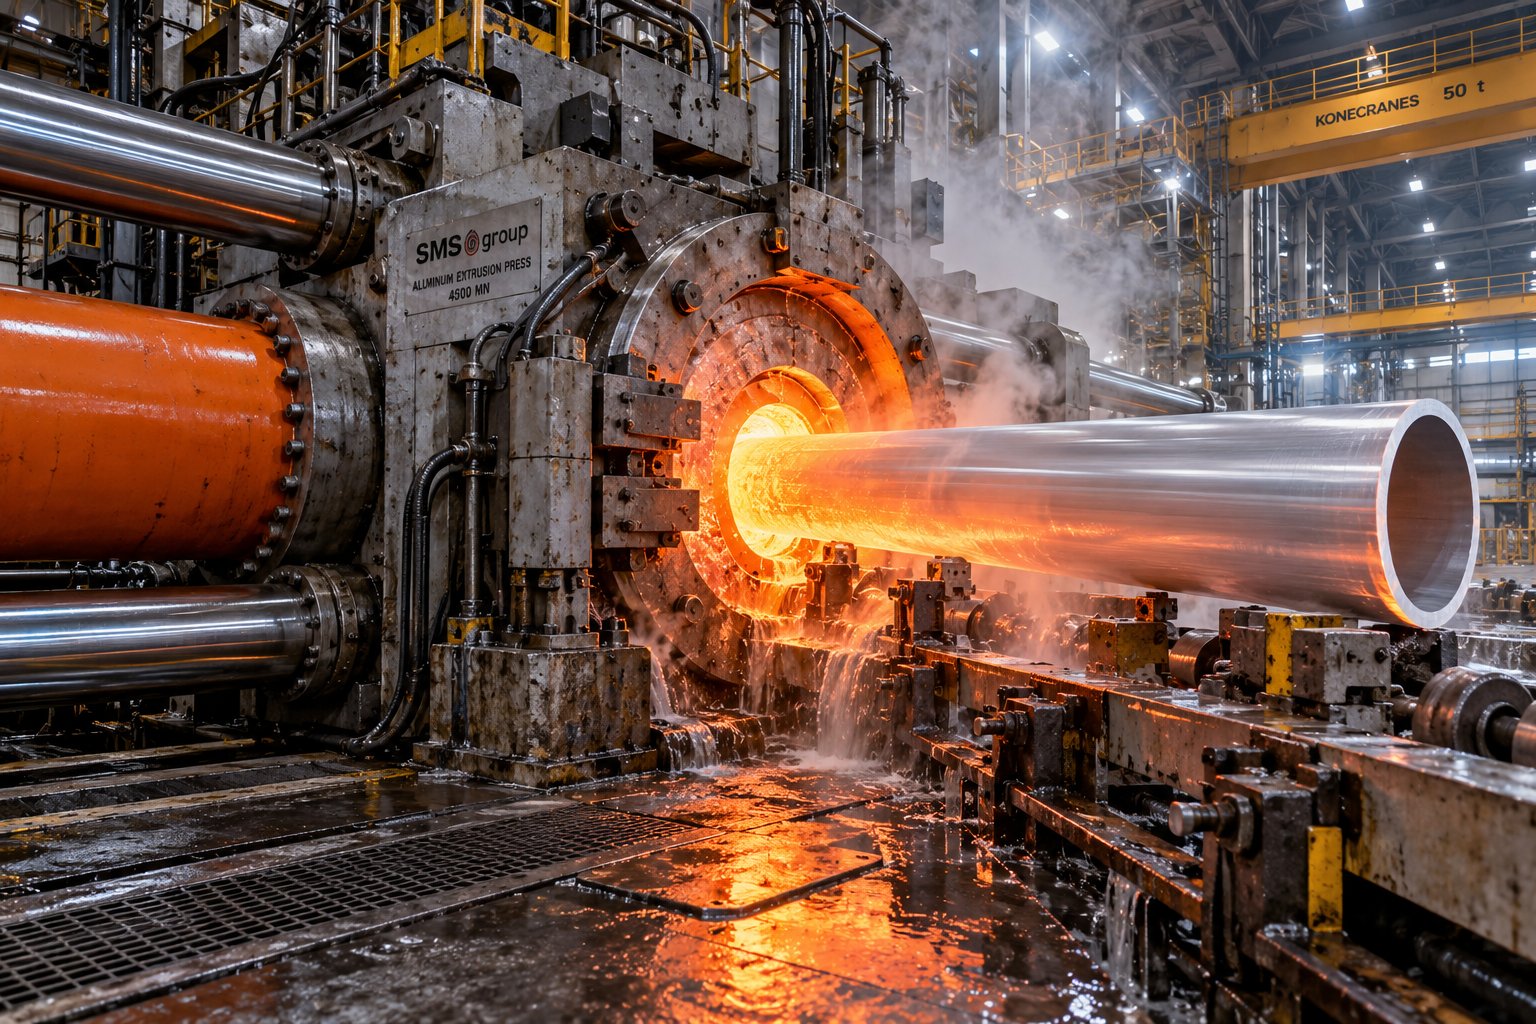
Imagine squeezing toothpaste through a tube opening. The paste emerges in the exact shape of that opening every single time. Aluminum tube extrusion works on precisely this principle, only with massive hydraulic presses generating up to 15,000 tons of pressure and temperatures reaching 500°C.
At its core, this manufacturing process involves forcing heated aluminum billets through a specially designed die to create hollow tubular profiles with remarkable precision. The result? Extruded aluminum tube products featuring consistent wall thickness, excellent dimensional accuracy, and superior mechanical properties that other manufacturing methods simply cannot match.
The transformation begins long before aluminum touches the extrusion press. First, a cylindrical billet gets cut from an elongated log of aluminum alloy material. This billet then enters a preheating oven where temperatures climb to 400-500°C. Why this specific range? The aluminum needs to become malleable enough for shaping while remaining solid, not molten.
While the billet heats, technicians preheat the die itself to 450-500°C. This critical step ensures even metal flow and extends die longevity. After applying lubricant to prevent the billet and ram from fusing together, the softened aluminum transfers mechanically into the press container.
Here is where the magic happens. The hydraulic ram applies tremendous pressure, pushing the malleable aluminum until it completely fills the container walls. With nowhere else to go, the material flows through the die opening, emerging as a fully-formed extruded tube on the other side.
The die essentially acts as the blueprint for your final product. For hollow profiles like tubes, manufacturers use specialized tooling that creates the interior void while simultaneously shaping the exterior. As the aluminum extrusion exits the press, a puller grasps it to maintain alignment while the profile undergoes quenching through water baths or forced air cooling.
Temperature control remains essential throughout. Even after quenching, the extrusions are not fully cooled. They transfer to a cooling plain until reaching room temperature, then undergo stretching to correct any twists and achieve final specifications. Finally, sawing cuts the profiles to length before heat treatment achieves the desired temper.
Tube extrusion dominates hollow profile manufacturing because it aligns the aluminum grain structure along the tube axis, delivering superior strength and ductility that casting, rolling, or drawing simply cannot replicate with the same consistency.
How does this compare to alternatives? Unlike casting, which can introduce porosity and inconsistent grain structure, extrusions maintain uniform mechanical properties throughout. Rolling works well for large-diameter tubes but struggles with thin walls and complex shapes. Cold drawing achieves excellent surface finish but reduces ductility and cannot produce the complex cross-sections that extruded aluminum handles effortlessly.
The bottom line? When you need hollow aluminum profiles with consistent wall thickness, complex geometries, and reliable performance, aluminum extrusion stands as the manufacturing method of choice across industries worldwide.
You have selected aluminum tube extrusion as your manufacturing method. But which aluminum alloy should you specify? This decision directly impacts strength, corrosion resistance, surface finish quality, and ultimately project success. The 6000 series dominates the aluminum tubing market for good reason, with two alloys standing above the rest: 6061 and 6063.
Both belong to the same alloy family, sharing magnesium and silicon as primary alloying elements. Yet their subtle compositional differences create distinct performance characteristics that make each better suited for specific applications. Understanding these differences helps you match material selection to your exact requirements.
Often called "architectural aluminum," 6063 is the most popular aluminum alloy for extrusions worldwide. Why? It has been optimized specifically for extrudability, producing aluminum round tubing and profiles with exceptionally smooth surface finishes. According to Gabrian, this alloy contains 0.45-0.9% magnesium and 0.2-0.6% silicon, lower concentrations than its 6061 counterpart.
This leaner composition translates to practical advantages. Alloy 6063 allows 25-35% thinner walls than 6061, making it ideal for lightweight aluminium tube applications where weight savings matter. Its superior surface quality makes it the preferred choice for anodized aluminum extrusions, accepting bright-dip anodizing to achieve highly reflective, mirror-like finishes.
In contrast, 6061 aluminum tubing earns its nickname as "structural aluminum" through higher strength ratings. With magnesium content between 0.8-1.2% and silicon at 0.4-0.8%, this alloy delivers significantly improved mechanical properties. Eagle Aluminum reports that 6061 T6 achieves ultimate tensile strength of at least 42,000 psi and yield strength of at least 35,000 psi. Compare this to 6063 T6 with ultimate tensile strength of 28,000 psi and yield strength of 23,000 psi.
What about 6005? This alloy bridges the gap between 6061 and 6063. It offers similar mechanical properties to 6061 tubing but with better extrudability and surface appearance. When your project demands high strength but also requires complex shapes or improved aesthetics, 6005 deserves serious consideration.
Sounds complex? Let's simplify the decision. Ask yourself: Is strength or surface finish more critical for your aluminum tube application?
When structural integrity takes priority, 6061 becomes your go-to choice. You'll find this alloy in:
When visual appeal and corrosion resistance matter more, 6063 excels. Common applications include:
| Alloy | Tensile Strength (T6) | Corrosion Resistance | Weldability | Best Applications |
|---|---|---|---|---|
| 6061 | 42,000+ psi | Good | Excellent | Structural components, marine parts, aerospace, bicycle frames |
| 6063 | 28,000+ psi | Very Good | Very Good | Architectural trim, window frames, furniture, decorative profiles |
| 6005 | 38,000+ psi | Good | Good | Complex structural shapes requiring better surface finish than 6061 |
Remember, temper treatment dramatically affects final properties regardless of which alloy you select. The T6 temper, involving solution heat treatment by artificial aging, maximizes strength in both 6061 and 6063. For applications requiring better formability at the expense of some strength, consider T4 or T5 tempers instead.
With alloy selection clarified, the next logical question becomes: what shape should your aluminum tube take? Round, square, and rectangular profiles each offer distinct advantages for different applications.
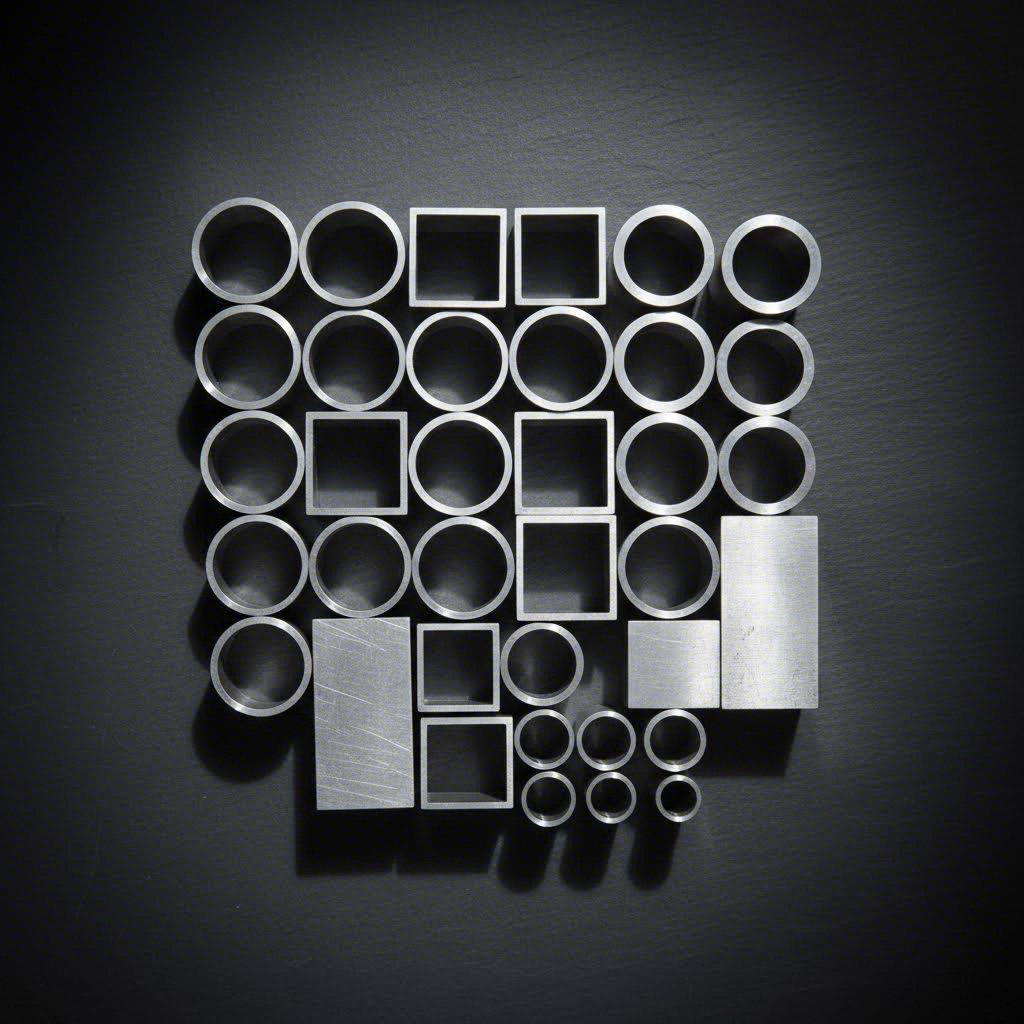
You have selected your aluminum alloy. Now comes an equally critical decision: which profile shape best serves your application? The geometry of your aluminum tube directly influences load-bearing capacity, connection methods, aesthetic appeal, and even manufacturing costs. Let's break down the three primary options and clarify exactly when each delivers optimal performance.
The aluminum round tube remains the most widely used profile shape across industries, and for good reason. Its circular cross-section distributes stress evenly around the entire circumference, making it exceptionally resistant to internal and external pressure loads.
What makes round tubing stand apart? Consider these key characteristics:
Where does round tubing excel? You will find it dominating applications like pressure vessels, hydraulic lines, handrails, conduit systems, heat exchangers, and bicycle frames. According to Alliance Tubular Products, round tubing provides better resistance to torsional forces than other shapes, making it suitable for trusses and frameworks where twisting stability matters most.
However, round profiles present challenges when connecting multiple tubes or mounting flat components. The curved surface requires specialized brackets, clamps, or welding techniques that angular profiles simply do not need.
When your project involves building frames, furniture, or structural assemblies, aluminum square tubing and rectangular aluminum tubing offer distinct advantages over round alternatives. Their flat surfaces and right-angle corners fundamentally change how you design, connect, and assemble components.
Why do engineers increasingly specify square aluminum tubing for framework applications? The answer lies in mechanical properties:
The aluminum rectangular tube takes these benefits further by offering directional strength characteristics. When loads primarily act in one direction, rectangular profiles concentrate material where you need it most. This makes them ideal for applications like architectural facades, window frames, solar panel mounting systems, and industrial machine frames.
According to Aluminium Warehouse, square and rectangular tubing are commonly referred to as "box section" and find extensive usage in architectural applications for their clean, modern aesthetic appeal. These shapes also excel in furniture production, shelving units, and modular display systems.
| Shape Type | Common Dimensions | Primary Advantages | Typical Uses |
|---|---|---|---|
| Round Tube | 6mm to 152.4mm (6") diameter; various wall thicknesses | Even pressure distribution, torsional strength, easy bending, optimal fluid flow | Pressure vessels, handrails, conduit, heat exchangers, bicycle frames, tent poles |
| Square Tube | 12.7mm (½") to 200mm width; standard 5m production lengths | Higher moment of inertia, easy connections, precise alignment, design flexibility | Structural framing, furniture, modular displays, guardrails, machine frames |
| Aluminum Rectangle Tube | Various aspect ratios from 1.5" x 2" to 4" x 6" | Directional strength, flush mounting, maximized stiffness in primary load direction | Architectural facades, window frames, solar panel mounts, industrial frames, wall-mounted displays |
So which shape should you choose? Consider these decision factors:
Real-world evidence supports these guidelines. The Shard in London uses square and rectangular tubing in its framework specifically because these shapes handle the building's immense vertical loads while simplifying connection details. Meanwhile, Boeing's 787 Dreamliner incorporates round tubing in areas requiring pressure containment and torsional stability.
Understanding shape selection is just the beginning. Once you know which profile suits your application, the next step involves specifying exact dimensions, wall thicknesses, and tolerances that ensure your extruded aluminum tubes perform precisely as intended.
You have selected your alloy and profile shape. Now comes the question that determines whether your aluminum tubes actually fit your application: what exact dimensions do you need? Reading tube specifications correctly prevents costly mistakes, production delays, and assembly failures. Let's decode the language of aluminum tube sizes and understand what those numbers really mean.
Every aluminum tube specification includes three critical measurements: outside diameter (OD), inside diameter (ID), and wall thickness. Understanding how these relate to each other helps you communicate precisely with suppliers and verify incoming materials.
The relationship is straightforward: Wall Thickness = (OD - ID) ÷ 2. If a tube measures 2 inches OD with a 1.5-inch ID, the wall thickness equals 0.25 inches. Suppliers typically specify two of these three dimensions, and you calculate the third. Most commonly, you will see OD and wall thickness listed, from which you derive the ID.
What aluminum tubing sizes are actually available? The market offers remarkable variety:
According to the Aluminum Association standards, extruded tube dimensions depend heavily on the circumscribing circle diameter, which is the smallest circle that completely encloses the tube's cross-section. Larger circumscribing circles generally allow for wider dimensional tolerances.
For most commercial applications, you will find standard lengths of 12, 20, or 24 feet, though custom cutting is widely available. Length tolerances typically run +1/8 inch for tubes up to 12 feet, increasing to +1/2 inch for lengths over 30 feet.
Wall thickness dramatically affects both strength and weight. But how thin can you go, and when should you choose thick wall aluminum tubing instead?
Thin wall aluminum tubing, generally defined as walls under 0.065 inches, offers significant weight savings for applications where structural demands are moderate. You will find thin wall aluminum pipe in furniture frames, display systems, lightweight enclosures, and decorative trim. The trade-off? Reduced load-bearing capacity and increased susceptibility to denting during handling.
Thick wall aluminum tubing, with walls exceeding 0.250 inches, handles heavy structural loads, pressure containment, and severe impact resistance. Applications include hydraulic systems, heavy machinery frames, marine components, and aerospace structural members. The penalty here is increased weight and material cost.
Tolerance classes determine how precisely your tubes will match specified dimensions. According to industry standard tolerance tables, extruded aluminum tubes follow these typical allowable deviations:
| Specified Diameter (inches) | Mean Diameter Tolerance (± inches) | Diameter at Any Point Tolerance (± inches) |
|---|---|---|
| 0.500 - 0.999 | 0.010 | 0.020 |
| 1.000 - 1.999 | 0.012 | 0.025 |
| 2.000 - 3.999 | 0.015 | 0.030 |
| 4.000 - 5.999 | 0.025 | 0.050 |
| 6.000 - 7.999 | 0.035 | 0.075 |
Wall thickness tolerances for round extruded tubes vary by both wall thickness and outside diameter. For tubes under 5 inches OD with walls between 0.125-0.249 inches, expect tolerances of ±0.009 inches on mean wall thickness. Larger tubes and thicker walls allow proportionally wider tolerances.
Why do tolerances matter? Consider a press-fit application where your tube must slide into a precision bore. If the tube's actual diameter falls at the high end of its tolerance range while the bore sits at the low end, assembly becomes impossible. Conversely, excessive clearance creates loose, rattling joints.
For critical applications, you can specify precision tolerances that tighten allowable deviations to approximately 65% of standard values. This precision comes at added cost, so reserve it for applications that genuinely require it.
Beyond diameter and wall thickness, straightness tolerances control how much a tube can deviate from a perfectly straight line. Standard tolerances allow 0.0125 inches of deviation per foot of measured length for most tempers. Softer tempers like O (annealed) permit greater deviation, up to 0.050 inches per foot.
An aluminum rectangular tubing sizes chart becomes essential when specifying non-round profiles. Width and depth tolerances follow similar patterns to round tubes, with standard tolerances ranging from ±0.012 inches for dimensions under 0.250 inches to ±0.054 inches for dimensions between 6-8 inches.
Armed with this dimensional knowledge, you can now specify aluminum tube dimensions with confidence. But knowing the right size is only part of the equation. Understanding where these tubes excel in real-world applications reveals why proper specification matters so much.
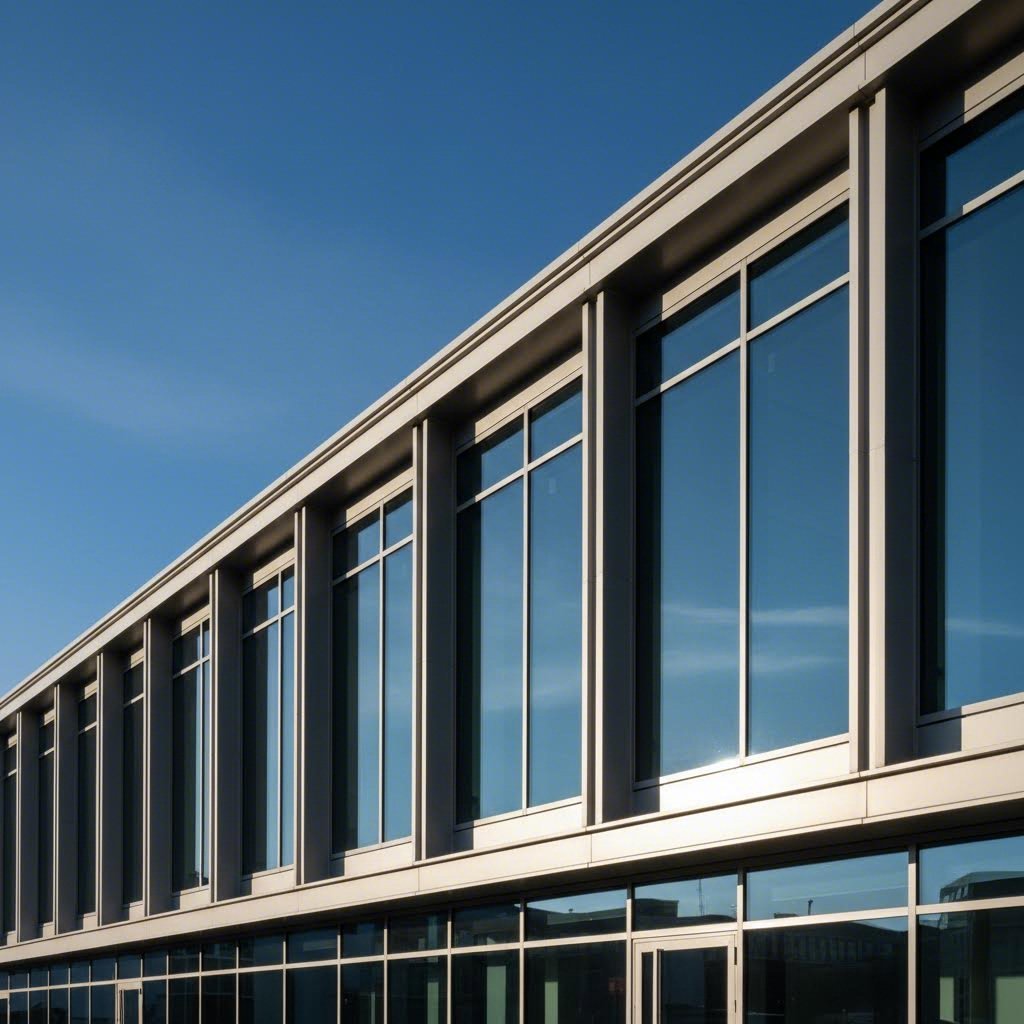
Why do engineers across virtually every industry reach for extruded aluminum profiles when designing their next product? The answer lies in a rare combination of properties: exceptional strength-to-weight ratio, natural corrosion resistance, and design flexibility that few other materials can match. From aircraft soaring at 35,000 feet to the furniture in your living room, aluminum tubes and aluminum extrusions have become indispensable across an astonishing range of applications.
Let's explore the specific industries where these versatile profiles deliver the greatest value and understand exactly why they've become the material of choice.
The transportation industry was among the first to recognize aluminum's game-changing advantages. When every pound matters, extruded aluminum profiles deliver unmatched performance.
In aerospace applications, you will find aluminum extrusion tube components throughout modern aircraft:
According to AMSpec, aerospace-grade alloys like 2024-T3, 7075-T6, and 7050-T76 meet the rigorous standards required for flight safety, fatigue resistance, and long-term corrosion resistance. The indirect extrusion process provides superior concentricity and surface quality that these demanding applications require.
The automotive sector has embraced aluminum with equal enthusiasm, particularly as electric vehicles demand weight reduction to maximize battery range:
Beyond cars and aircraft, personal mobility devices rely heavily on extruded aluminum. Bicycle suspension tubes, seat posts, motorcycle handlebars, and wheelchair frames all benefit from thin-walled drawn tubes that minimize weight while maximizing strength.
Walk through any modern building and you're surrounded by aluminum extrusions. The construction industry has adopted these profiles for applications ranging from structural frameworks to decorative trim.
Key architectural applications include:
Why does construction favor aluminum over steel or other metals? The answer goes beyond weight savings. Aluminum naturally forms a protective oxide layer that resists corrosion without painting or galvanizing. This self-protecting characteristic dramatically reduces maintenance costs over a building's lifetime, especially in coastal or industrial environments where corrosive elements accelerate steel degradation.
Industrial equipment manufacturers specify aluminum tubes for applications where reliability and performance matter most:
Consumer products represent another massive market for extruded aluminum. You will encounter these profiles in:
Aluminum can be recycled repeatedly without losing its mechanical properties, making it one of the most sustainable material choices for manufacturers committed to environmental responsibility.
This sustainability advantage increasingly drives specification decisions across all industries. According to industry sources, recycled aluminum requires only 5% of the energy needed to produce primary aluminum, yet delivers identical performance characteristics.
Understanding where aluminum tubes excel is valuable knowledge. But knowing how to select the right specifications for your specific project transforms that knowledge into practical results. The next section guides you through a systematic approach to matching tube specifications with your exact requirements.
You understand alloys, shapes, and dimensions. But how do you bring all this knowledge together to specify the perfect aluminum tube for your project? Without a systematic approach, even experienced engineers can overlook critical factors that lead to underperforming components or costly overspecification.
The selection process doesn't need to be overwhelming. Follow this step-by-step framework, and you'll confidently match aluminum extrusion shapes to your exact requirements every time.
When your aluminum extruded tube must bear loads, accurate calculations become non-negotiable. According to structural engineering guidelines, the load-carrying capacity depends on material properties, cross-sectional geometry, connection methods, and environmental factors working together.
Start with the basics: calculate your tube's cross-sectional area and moment of inertia. For square tubes, the moment of inertia follows the formula I = (a⁴ - b⁴) / 12, where "a" represents the outer dimension and "b" represents the inner dimension. These values determine how much bending stress the tube can handle before deformation occurs.
Next, verify that compressive or tensile stress remains below the allowable stress for your selected alloy. For 6061-T6 aluminum, the yield strength of 35,000 psi establishes your upper limit with appropriate safety factors applied. Typical structural applications use safety factors between 1.5 and 3.0 depending on consequence of failure.
Don't forget stability checks for long or thin tubes. Euler's buckling formula (Pcr = π²EI / L²) helps determine critical loads where slender columns might buckle before reaching material yield strength. Here, E represents the elastic modulus (approximately 10,000 ksi for aluminum), I is moment of inertia, and L is the effective column length based on end conditions.
How the tubing connects matters tremendously. Good welding maintains structural integrity, while poor welds create failure points. For bolted connections, verify that fastener spacing and edge distances meet aluminum design standards to prevent tearout failures.
Your operating environment influences alloy selection as much as mechanical requirements do. According to corrosion resistance research, different metals react differently to moisture, chemicals, and temperature exposure based on the protective oxide layers they form.
Aluminum naturally forms a thin, stable oxide film that seals the surface against further corrosion. However, certain environments compromise this protection:
Temperature also affects load capacity directly. Elevated operating temperatures reduce aluminum's strength significantly, while cold environments may affect ductility. Factor these conditions into your stress calculations with appropriate derating factors.
The best tube specification isn't the strongest or most corrosion-resistant option available—it's the one that precisely matches your application requirements without unnecessary cost or weight penalty.
Standard aluminum pipe sizes offer the best combination of availability and economy. Before specifying custom dimensions, verify whether your requirements can be met with standard aluminum extrusions that suppliers stock regularly. Custom dies and non-standard profiles add cost and extend lead times, though they become worthwhile when standard options genuinely cannot meet your needs.
With specifications determined, your next consideration becomes surface treatment. The right finish transforms raw aluminum into a component ready for its intended environment, whether that means enhanced corrosion protection, specific aesthetic requirements, or improved wear resistance.
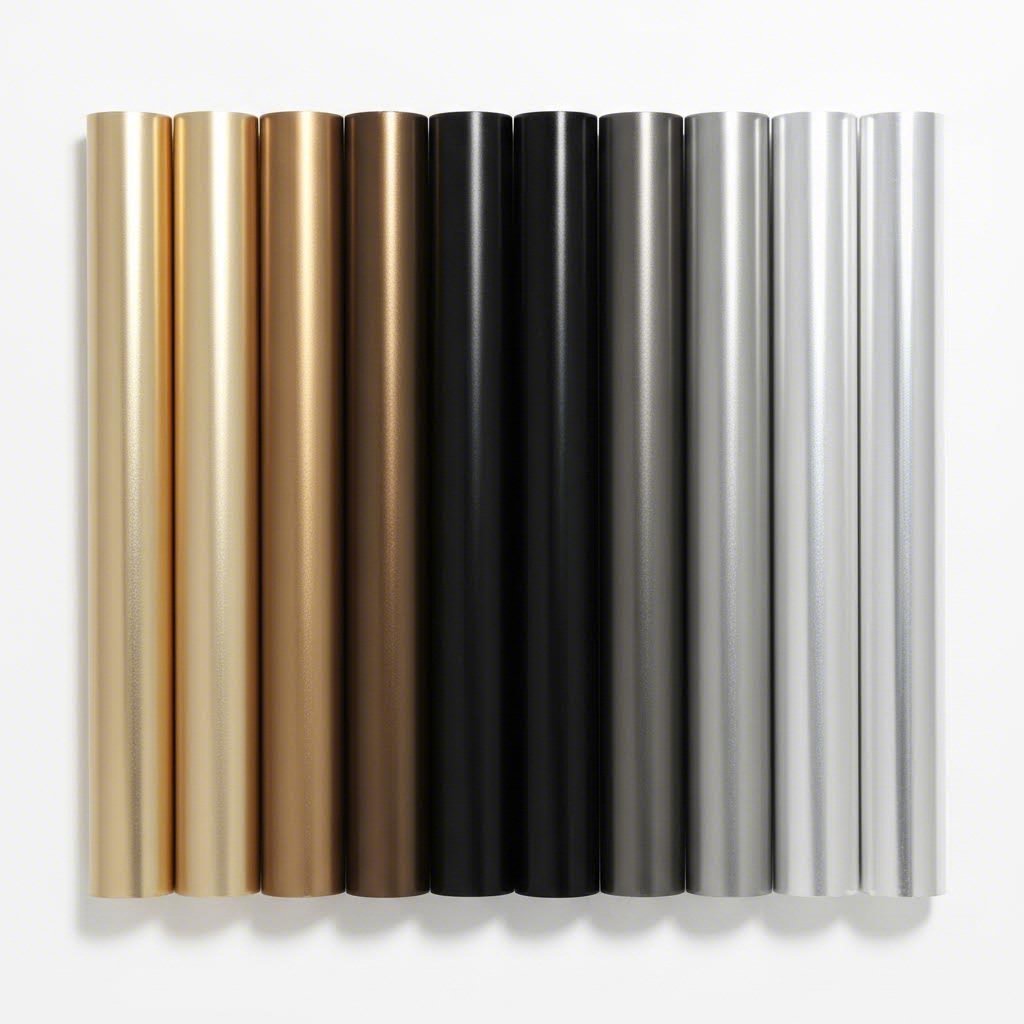
Your aluminum extrusion profile emerges from the press with what manufacturers call a "mill finish." This raw state shows die marks, slight oxidation, and a dull appearance that rarely suits finished products. The right surface treatment transforms this basic starting point into a component that resists corrosion, wears beautifully, and performs reliably for decades.
Why invest in surface finishing? According to Gabrian, the right surface finish can elevate products from "good" to "outstanding" by improving corrosion resistance, wear resistance, and aesthetic appearance. Mill finish aluminum only makes sense for the cheapest applications where appearance doesn't matter and short service life is acceptable.
Let's explore the primary finishing options available for your extruded aluminium tubes and understand when each delivers optimal value.
Anodizing stands as the most popular finishing method for aluminium extrusion components, and with good reason. Unlike paints or coatings that apply external layers, anodizing uses an electrochemical process to grow the aluminum's naturally-occurring oxide layer into a thicker, harder protective barrier.
What makes anodized finishes exceptional? The process creates an integral part of the aluminum itself rather than a separate coating that might chip or peel. This oxide layer delivers:
According to Worthwill Aluminium, the anodizing yield level directly affects final product cost, with proper control of oxidant concentration, temperature, and current density being critical to success. Two-color anodizing processes even allow different colors on different surfaces of the same profile.
The trade-off? Color options, while varied, remain more limited than powder coating. And the process works best with certain alloys, with 6063 being particularly well-suited for bright-dip anodizing that creates highly reflective, mirror-like finishes.
When your project demands vibrant colors, specific RAL matches, or textures that anodizing cannot achieve, powder coating becomes the go-to solution. This process electrostatically applies dry paint powder to prepared aluminum surfaces, then bakes the parts to melt and cure the coating into a durable finish.
Powder coating offers distinct advantages for aluminum t extrusion components:
However, powder coatings lack the hardness of anodized surfaces. Physical damage can expose underlying aluminum, making touch-up repairs necessary in demanding applications.
Beyond these primary options, specialty finishes address specific performance requirements:
| Finish Type | Corrosion Resistance | Hardness | Color Options | Best Applications |
|---|---|---|---|---|
| Anodizing | Excellent | Very High | Limited (metallic tones, black) | Architectural trim, aerospace components, wear surfaces |
| Powder Coating | Very Good | Moderate | Unlimited | Furniture, decorative elements, color-critical applications |
| PVDF | Excellent | Good | Wide range (matte finish) | Exterior cladding, curtain walls, harsh weather exposure |
| Micro-arc Oxidation | Excellent | Superior | Limited | High-wear components, thermal barriers, premium applications |
How do surface treatments affect your final application? Consider the complete service environment. Marine installations benefit from anodizing's integral oxide barrier. Architectural facades exposed to UV radiation and weather extremes perform best with PVDF. Interior furniture and display systems where appearance matters most often specify powder coating for its color flexibility.
Manufacturers offering comprehensive finishing capabilities provide significant advantages for complex projects. Rather than coordinating between extrusion suppliers and separate finishing houses, working with an integrated supplier like Shengxin Aluminium streamlines the process. Their facilities handle everything from anodizing in custom colors like champagne and rose gold, to powder coating, PVDF application, and micro-arc oxidation, delivering end-to-end solutions under one roof.
With surface treatment options clarified, one critical question remains: where should you source your aluminum tubes to ensure quality, competitive pricing, and reliable delivery?
You have nailed down your alloy, profile shape, dimensions, and surface finish. Now comes a decision that determines whether your project succeeds or stumbles: where do you actually buy aluminum tubing? The supplier you choose affects everything from product quality and lead times to total project costs and technical support when challenges arise.
Finding aluminum extrusions for sale is easy. Finding a supplier who delivers consistent quality, competitive pricing, and genuine technical partnership? That requires knowing what to look for and which questions to ask. Let's break down the evaluation process so you can source extruded aluminum tubing with confidence.
Not all aluminum extrusion suppliers are created equal. The difference between a basic supplier and a comprehensive manufacturing partner often comes down to equipment capabilities and in-house resources. When evaluating potential suppliers for your aluminum tube stock needs, focus on these critical factors:
According to American Douglas Metals, in-house capabilities mean the manufacturer can oversee the entire production journey, from blueprint design to meticulous surface finishing touches. This hands-on approach ensures the resultant aluminum extrusion profile aligns seamlessly with your stipulations, curbing chances of miscommunication or undue delays.
What happens when suppliers lack these capabilities? Engaging with manufacturers who outsource critical operations can result in varying quality levels and additional costs. When challenges arise, having multiple intermediaries makes troubleshooting a cumbersome affair.
When standard profiles don't meet your requirements, custom extrusion becomes necessary. This is where die development support separates exceptional suppliers from adequate ones.
The extrusion die essentially acts as the blueprint for your final product. Creating a new die requires precision engineering, specialized tooling equipment, and deep understanding of how aluminum flows through complex geometries. Suppliers with robust die development capabilities can:
Why does this matter? Manufacturers with limited experience might lead to subpar products or hitches during the manufacturing phase. Such hurdles might trigger delays, escalating costs, and a final product that falls short of your aspirations.
Factory-direct pricing represents another significant advantage when you buy aluminum tube directly from manufacturers rather than through distributors. Eliminating middlemen reduces costs while providing direct communication channels to the people actually producing your parts. When questions arise about tolerances, finishes, or delivery schedules, you're speaking with the source rather than playing telephone through intermediaries.
For projects requiring comprehensive aluminum extrusion supply capabilities, Shengxin Aluminium exemplifies what a full-service partner looks like. Their facility houses 35 extrusion presses ranging from 600T to 5500T, providing capacity for everything from delicate architectural trim to heavy structural sections. State-of-the-art CNC machining centers handle precise cutting, drilling, and bending to exact specifications. Their surface treatment options span anodizing in custom colors including champagne and rose gold, powder coating, PVDF, and micro-arc oxidation for superior durability.
Most importantly, their technical team provides end-to-end support from die development through mass production. With over 30 years of industry experience, they've navigated the challenges that trip up less experienced suppliers, positioning them to deliver solutions rather than excuses when your project demands precision extruded aluminum for sale.
Before committing to any supplier for aluminum tubing for sale, verify these critical details:
Picking a manufacturer based merely on cost could expose you to inferior products and lackluster customer service. Such compromises can elevate long-term costs due to early product wear or replacements.
The right supplier relationship extends beyond individual transactions. When you find a manufacturer who understands your industry, maintains consistent quality, and responds promptly to technical questions, you've gained a competitive advantage that pays dividends across every project you tackle together.
Hollow aluminum tubes are extruded using two primary methods: seamless and pressure welded. In the seamless method, a mandrel creates the internal void while the die shapes the exterior. For pressure welded extrusions, aluminum flows around internal bridges in the die and welds together under extreme pressure before exiting. The process starts with heating aluminum billets to 400-500°C, then forcing the softened metal through specialized dies using hydraulic presses generating up to 15,000 tons of pressure.
The key difference lies in strength versus surface finish quality. 6061 aluminum tubing offers higher tensile strength (42,000+ psi vs 28,000+ psi) making it ideal for structural applications like bicycle frames and aerospace components. 6063 aluminum provides superior extrudability and smoother surface finishes, making it the preferred choice for architectural applications, window frames, and decorative elements requiring anodizing. Both alloys offer good corrosion resistance and weldability.
Extruded aluminum tubes come in extensive size ranges. Round tubes span 0.500 inches to over 24 inches in outside diameter with wall thicknesses from 0.035 to 3.5 inches. Square tubes range from 0.5 to 12 inches per side with walls from 0.062 to 0.500 inches. Rectangular tubes vary from 0.5" x 1" up to 4" x 12" and beyond. Standard lengths typically include 12, 20, or 24 feet, though custom cutting is widely available from most suppliers.
Evaluate press capacity range (diverse presses from 600T-5500T accommodate various profile sizes), CNC machining capabilities for secondary operations, surface treatment options (anodizing, powder coating, PVDF), technical support depth for alloy and design guidance, and production volume flexibility. Comprehensive manufacturers like Shengxin Aluminium offer end-to-end services from die development through mass production, eliminating coordination between multiple vendors.
Common surface treatments include anodizing (creates integral oxide layer for corrosion resistance and accepts dyes for colors like champagne, bronze, and black), powder coating (unlimited color options with excellent durability), PVDF coatings (superior weather resistance for exterior applications), and micro-arc oxidation (ceramic surface for superior hardness). Each finish serves different performance and aesthetic requirements based on your application environment.


 บริการออนไลน์
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 ไทย
 English
 français
 Deutsch
 русский
 español
 português
 العربية
 Việt
 Українська