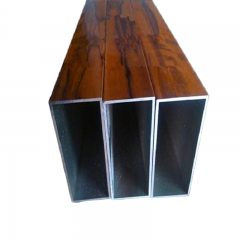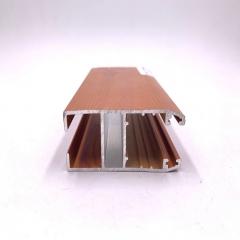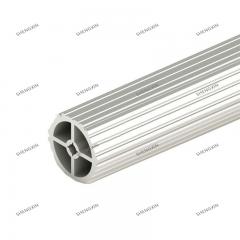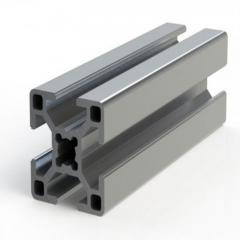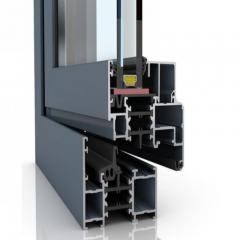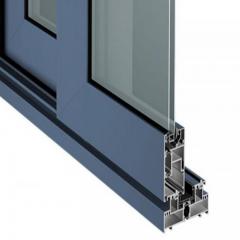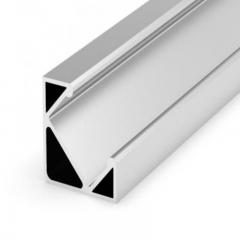
Ever wondered how factories build those sleek, modular workstations that seem to reconfigure overnight? Or how trade show booths appear and disappear like magic? The answer lies in aluminum frame extrusion profiles—precision-engineered structural components that have quietly revolutionized how we build everything from industrial machine frames to DIY 3D printer enclosures.
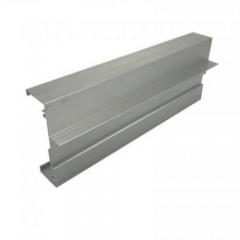
Aluminum frame extrusion profiles are standardized lengths of extruded aluminum featuring specialized channel designs that allow components to connect without welding, drilling, or permanent fastening. Think of them as adult-sized building blocks, but with the strength to support heavy machinery and the precision to meet engineering specifications.
What makes these profiles unique is their T-slot rail design—a series of T-shaped channels running along the profile's length. These channels accept specialized hardware like T-nuts and brackets, enabling connections at virtually any point. You can assemble an entire workstation in hours, then disassemble and reconfigure it next month when your needs change.
The aluminum extrusion process transforms solid metal into complex shapes through a surprisingly elegant method. Here's how it works:
First, manufacturers cut cylindrical billets from aluminum logs and preheat them to 400-500°C. This temperature makes the metal malleable without melting it—imagine the consistency of firm clay. Meanwhile, a custom-designed die (essentially a steel template of the desired cross-section) preheats to 450-500°C to ensure even metal flow.
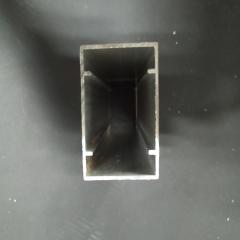
Next comes the impressive part. A hydraulic ram applies up to 15,000 tons of pressure, forcing the softened billet through the die opening. The aluminum extruded through this process emerges fully formed with the exact cross-sectional shape of the die—whether that's a simple square tube or a complex profile with multiple T-slots and internal chambers.
After extrusion, the profiles undergo quenching (rapid cooling), stretching to correct any twists, and cutting to standard lengths. Heat treatment finalizes the aluminum's mechanical properties, resulting in lightweight yet remarkably strong structural components.
The genius of aluminum extrusion lies not just in the manufacturing process, but in what it enables: a construction system where every connection point is also an adjustment point, eliminating the permanence that makes traditional metal fabrication so inflexible.
This extrusion extrusion process produces profiles with exceptional consistency—each meter of aluminum extrusion profiles matches the next with precision tolerances. That consistency is what makes modular systems possible, allowing components from different production runs to connect seamlessly.
Understanding these fundamentals isn't just academic. When you browse supplier catalogs filled with series numbers and slot dimensions, knowing what extruded aluminum actually is—and how T-slot systems work—helps you make informed decisions rather than guessing at specifications.
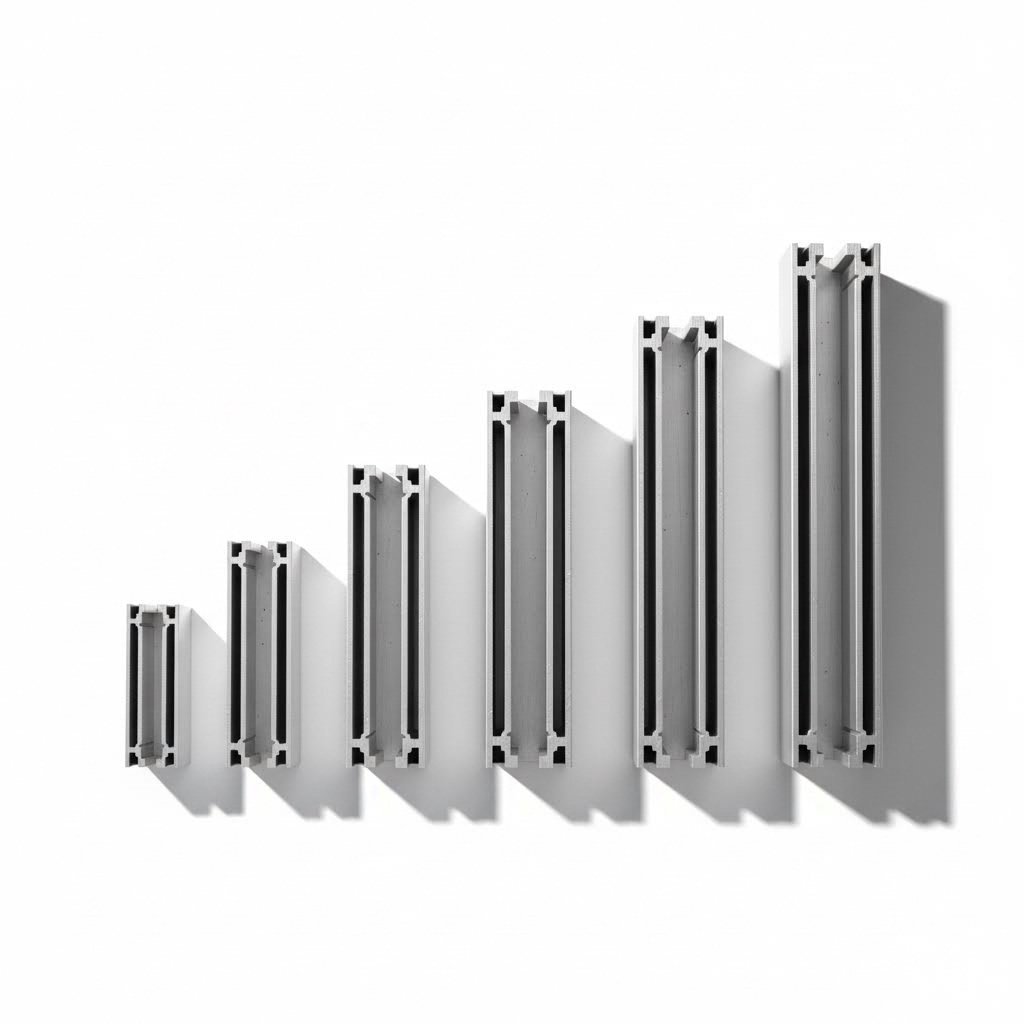
You've probably seen specifications like "40 Series" or "80/20 aluminum" scattered across supplier websites. But what do these numbers actually mean? If you've ever felt confused browsing aluminum extrusion profile catalogs, you're not alone—most suppliers reference these series classifications without explaining them.
Here's the simple truth: series numbers typically correspond to the profile's outer dimension in millimeters. A 40 Series profile measures 40mm x 40mm in its basic square configuration. A 20 Series profile? That's 20mm x 20mm. Once you understand this principle, navigating aluminum extrusion sizes becomes far less intimidating.
The series system extends beyond simple squares. Within each series, you'll find rectangular variations like 20 x 40 or 40 x 20 profiles—same slot compatibility, different structural properties. A 20 x 40 profile offers greater rigidity in one direction, making it ideal when loads primarily travel along a single axis. Similarly, a 15 x 40 configuration provides options for applications needing compact width with extended height.
The 80 20 aluminum name you've likely encountered comes from a popular manufacturer, but it also references their fractional-inch system—where profiles measure in inch increments rather than metric. This brings us to an important regional distinction.
The aluminum extrusion profile world operates on two parallel sizing systems:
These systems are fundamentally incompatible. A metric 4040 profile won't accept hardware designed for a 1.5" fractional series, even though they appear similar in size. The slot geometries, fastener threads, and accessory dimensions differ entirely. When sourcing components, commit to one system throughout your project.
For conversion reference: 25.4mm equals 1 inch. A 40mm profile approximates 1.57 inches, while a standard 1.5" fractional profile equals 38.1mm. Close—but not interchangeable.
| Series Name | Profile Dimension | Slot Width | Typical Applications | Weight Considerations |
|---|---|---|---|---|
| 15 Series | 15mm x 15mm | 5mm | Lightweight frames, 3D printer enclosures, small fixtures | ~0.3 kg/m - Ultra-light, limited load capacity |
| 20 Series | 20mm x 20mm | 5-6mm | Electronics enclosures, light guarding, prototyping | ~0.5 kg/m - Good for light-duty applications |
| 30 Series | 30mm x 30mm | 8mm | Workstations, medium frames, display structures | ~0.9 kg/m - Balanced strength and weight |
| 40 Series (4040) | 40mm x 40mm | 8mm | Machine frames, safety guards, conveyor systems | ~1.5 kg/m - Industrial standard, excellent rigidity |
| 45 Series | 45mm x 45mm | 10mm | Heavy machinery, structural bases, automation cells | ~1.9 kg/m - Enhanced load capacity |
| 80 Series | 80mm x 80mm | 10mm | Heavy-duty structures, large machine bases, gantries | ~4.5 kg/m - Maximum strength for demanding applications |
Notice how slot width increases with profile size. This matters because larger slots accept heavier-duty fasteners, enabling stronger connections for the increased loads these profiles support. A 15 Series profile's 5mm slot simply cannot accommodate the robust hardware needed for heavy industrial applications.
The 4040 designation you'll frequently encounter is shorthand for 40mm x 40mm—the workhorse of industrial aluminum framing. This series strikes an optimal balance between structural capability and cost-effectiveness, explaining its popularity across machine frames, workstations, and safety enclosures.
When selecting your series, consider not just the load requirements but also the accessory ecosystem. Larger series offer more hardware options, while smaller series might limit your choices for specialized connectors and brackets. This hardware compatibility becomes crucial as we explore how T-slot geometry enables the modular connections that make these systems so versatile.
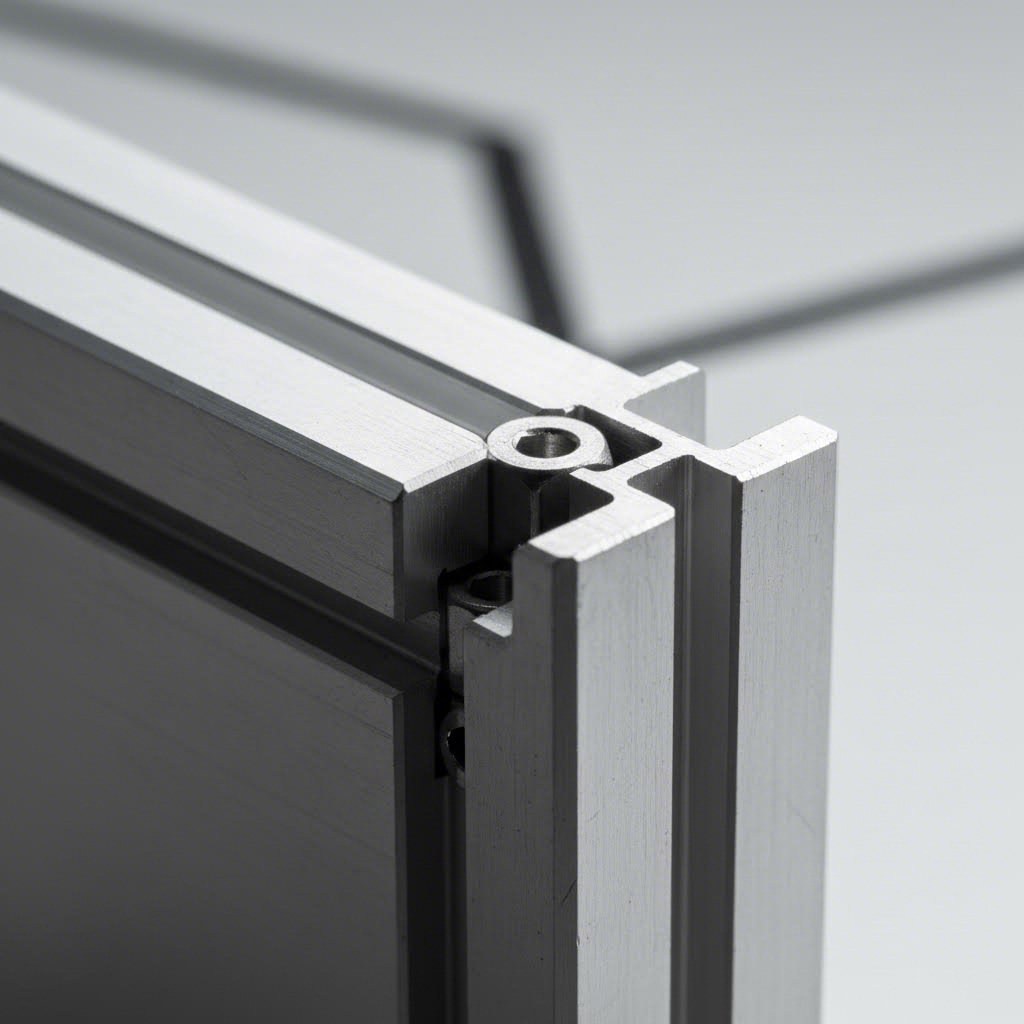
What makes one piece of aluminum connect to another without welding, drilling, or permanent fasteners? The answer lies in a deceptively simple geometric feature that has transformed industrial construction. Understanding T-slot design isn't just technical knowledge—it's the key to unlocking the full potential of modular aluminum framing.
Imagine a channel shaped like an inverted "T" running the entire length of an aluminum profile. The narrow opening at the surface widens into a broader cavity beneath—creating a mechanical lock that captures specially designed fasteners. This t slotted aluminum design is the foundation of everything modular framing systems can accomplish.
Here's how the connection works: A T-nut—a fastener with a rectangular head sized to fit the slot's internal dimensions—slides into the channel through the narrow opening. Once inside, rotating the nut 90 degrees positions the head perpendicular to the slot opening. Now it's trapped. Tightening a bolt through an attached bracket or component pulls everything together, creating a rigid connection at any point along the profile's length.
The beauty of this system? You're not limited to pre-drilled holes. Every millimeter of that t slot rail becomes a potential connection point. Need to mount a sensor 47mm from the end? No problem. Want to shift that bracket 3mm to the left next week? Simply loosen, slide, and retighten.
The t channel aluminum design delivers advantages that traditional fabrication methods simply cannot match. Consider what happens when you need to modify a welded steel frame—you're looking at cutting, grinding, rewelding, and refinishing. With aluminum t slot systems, modifications take minutes instead of hours.
The extruded t slot system transforms structural assembly from a specialized trade into an accessible process. Anyone with a basic understanding of the components can build professional-grade frames, enclosures, and workstations.
You'll encounter two primary slot geometries in modular aluminum framing: T-slots and V-slots. While they share some compatible hardware, they serve distinct purposes.
T-slot profiles feature the rectangular channel we've described—optimized for structural connections using T-nuts, brackets, and fasteners. The geometry prioritizes secure mechanical locking and load-bearing capability. These tslots dominate industrial framing, machine bases, and safety enclosures.
V-slot profiles incorporate a beveled edge that creates a V-shaped groove. This geometry serves a specialized purpose: guiding wheels and bearings for linear motion systems. The angled surfaces allow rollers to sit precisely within the channel, effectively turning the profile into both structure and linear rail. A v slotted aluminum insert or dedicated V-slot profile can significantly reduce costs for CNC machines and 3D printers by eliminating separate linear guide components.
Can you use them interchangeably? For basic brackets and T-nuts, often yes. Both systems accept similar fastening hardware. However, for motion applications requiring wheels or bearings, the distinction matters significantly. V-slot's beveled geometry guides rolling components precisely, while t slotted designs lack the angled surfaces necessary for smooth linear travel.
Beyond slot geometry, profile shape dramatically influences structural performance. Manufacturers offer several configurations to address different engineering requirements:
Square Profiles (40x40, 30x30, etc.) provide equal rigidity in all directions. They're the default choice for general framing where loads distribute evenly or come from unpredictable directions. Most machine frames and enclosures start with square profiles as their foundation.
Rectangular Profiles (20x40, 40x80) offer asymmetric rigidity—greater resistance to bending along the longer axis. When you know your primary load direction, rectangular aluminum t channel profiles optimize material usage. A horizontal beam supporting vertical weight benefits from the added depth a 40x80 provides versus a 40x40.
Corner Profiles feature 90-degree configurations designed specifically for frame edges and enclosure corners. They create clean exterior lines while providing interior T-slots for component attachment.
Specialty Profiles address unique requirements—rounded exteriors for safety in high-traffic areas, profiles with integrated wire channels, or heavy-wall versions for extreme loads. The extrusion process allows virtually unlimited cross-sectional designs.
Understanding how these shapes work together—with t slot rail connections enabling modular assembly—reveals why this system has become the industrial standard. The combination of geometric flexibility, tool-free reconfiguration, and reusable components creates possibilities that welded fabrication simply cannot match. But selecting the right profile involves more than just shape—the aluminum alloy itself significantly impacts performance, durability, and cost.
You've selected your profile series and understand how T-slot connections work. But here's a question most suppliers never address: what's the aluminum itself actually made of? Not all extruded metal is created equal, and the alloy composition significantly impacts everything from structural strength to how well your profiles accept anodized aluminum finishes.
When browsing aluminium extrusion catalogs, you'll encounter two alloy designations repeatedly: 6063 and 6061. Both belong to the 6000-series aluminum family, alloyed primarily with magnesium and silicon. But their performance characteristics differ enough to matter for your project.
6063 Aluminum is the industry standard for architectural and general-purpose framing. Why? It extrudes beautifully. The alloy flows smoothly through complex dies, producing crisp corners and consistent wall thicknesses. According to Howard Precision Metals, 6063 is the most popular extruded aluminium alloy specifically because of its ease of extrudability and exceptional surface finish quality.
This alloy also accepts surface treatments exceptionally well. Whether you're acid etching for a matte appearance or bright dip anodizing for maximum reflectivity, 6063 delivers consistent, attractive results. For visible applications—think display fixtures, architectural trim, or customer-facing enclosures—this matters tremendously.
6061 Aluminum trades some of that surface perfection for significantly higher strength. This precipitation-hardened alloy undergoes heat treatment that disperses particles throughout its grain structure, preventing displacement and increasing durability. When structural demands exceed what 6063 can handle, 6061 becomes the go-to choice.
Sounds technical? Let's break down the practical differences. The table below compares the properties that actually affect your project decisions:
| Property | 6063-T6 Aluminum | 6061-T6 Aluminum |
|---|---|---|
| Ultimate Tensile Strength | At least 28,000 psi | At least 42,000 psi |
| Yield Strength | At least 23,000 psi | At least 35,000 psi |
| Corrosion Resistance | Excellent | Excellent |
| Weldability | Good (loses ~30% strength when welded) | Good (strength recoverable with heat treatment) |
| Surface Finish Quality | Exceptional—smooth, uniform appearance | Good—slightly less refined than 6063 |
| Extrudability | Excellent—ideal for complex shapes | Good—but less suited to intricate profiles |
| Machinability | Fair | Good—easier secondary machining |
| Anodizing Response | Superior—consistent, attractive finishes | Good—functional but less cosmetically refined |
| Typical Applications | Window frames, architectural trim, display fixtures, furniture, tubing | Structural angles, aircraft parts, bicycle frames, hydraulic manifolds, heavy-duty supports |
Notice the strength differential. The 6061 alloy delivers roughly 50% higher tensile and yield strength compared to 6063. For an aluminum plate supporting heavy machinery or a structural frame bearing significant loads, that difference can determine whether your design succeeds or fails.
So how do you choose? Consider these practical guidelines:
Choose 6063 when:
Choose 6061 when:
Here's the reality most suppliers won't tell you: for the vast majority of aluminum frame extrusion profile applications, 6063 performs perfectly well. The modular framing systems we've discussed—workstations, enclosures, machine frames—typically specify 6063 as standard. You're not compromising by choosing it; you're selecting the alloy specifically engineered for these applications.
Reserve 6061 for situations where engineering calculations specifically demand higher strength, or where safety factors require additional margin. The higher material cost and potentially longer lead times for 6061 profiles should be justified by genuine structural requirements, not just a preference for "stronger" materials.
Both alloys share excellent corrosion resistance—a defining characteristic of the 6000-series family. For most indoor and outdoor applications, either choice provides decades of service without degradation. This durability foundation supports the next consideration in profile selection: matching the right size and shape to your specific load requirements.
You understand the alloys. You know your series options. But here's where most buyers get stuck: how do you actually match a specific profile to your project's demands? Supplier catalogs list dozens of aluminum extrusion shapes, yet rarely explain which one you actually need. Let's fix that with a practical selection framework you can apply immediately.
The fundamental principle is straightforward: larger profiles and heavier wall thicknesses increase both rigidity and weight capacity. A 40x40mm profile handles loads that would bend a 20x20mm version. But "bigger is better" wastes money when lighter profiles would suffice.
Think about what "load" actually means for your application. Are you supporting static weight—like equipment sitting on a workbench? Or dynamic loads—forces from moving machinery, vibration, or impacts? Static loads are predictable. Dynamic loads require additional safety margins because forces can momentarily spike well above the average.
According to Wiley Metal, the cross-sectional shape significantly influences how extruded aluminum profiles resist different load types. Axial loads (tension or compression along the profile's length) depend primarily on material strength. But bending and torsional loads? Shape matters enormously there.
Rather than guessing or over-specifying, follow this systematic approach to profile selection:
When you know where your loads come from, rectangular profiles offer a significant advantage. Here's the physics in plain terms:
Square profiles—like your standard 4040—provide equal rigidity in all directions. They resist bending equally whether force comes from above, below, or the sides. This makes them ideal when load directions are unpredictable or when forces truly distribute evenly.
Rectangular aluminum extruded shapes concentrate material differently. A 40x80mm profile is substantially stiffer in the 80mm direction than a 40x40 profile, while using similar material volume. Think of it like an I-beam rotated 90 degrees—the extra depth resists bending more effectively.
Practical example: imagine a horizontal beam supporting vertical weight. A 40x80mm profile oriented with the 80mm dimension vertical will deflect significantly less than a 40x40mm profile under identical loading. You're getting more rigidity without proportionally more weight or cost.
But orientation matters critically. That same 40x80 profile turned sideways (80mm horizontal) performs worse than a 40x40 for vertical loads. Rectangular profiles optimize performance in one direction at the expense of others.
| Profile Type | Rigidity Characteristics | Best Applications | Avoid When |
|---|---|---|---|
| Square (40x40, 30x30) | Equal strength in all directions | General framing, unknown load directions, column supports | You know exactly where loads come from and can optimize |
| Rectangular (40x80, 20x40) | Maximum rigidity in one axis, reduced in the perpendicular axis | Horizontal beams with vertical loads, gantry rails, long spans | Multi-directional loads, torsional stress applications |
| Aluminum Angle | Rigidity concentrated at corner junction | Corner reinforcement, edge protection, light structural bracing | Primary load-bearing members, long unsupported spans |
The alum extrusion shapes you select should match your load profile, not just your budget. A properly specified rectangular profile often outperforms a heavier square profile while costing less—because you're placing material exactly where it's needed.
DIY project builders can often size profiles through experience and conservative estimation. But certain situations demand professional engineering consultation:
As CAN Art notes, tolerances and precision matter significantly for demanding applications like aerospace or automotive components—contexts where professional engineering review isn't optional.
Most modular framing projects—workstations, enclosures, display fixtures—fall comfortably within standard profile capabilities using conservative sizing. But recognizing when you've exceeded DIY territory protects both your project and your safety.
With profile selection principles established, the next consideration becomes equally practical: how will these profiles actually be used? Understanding real-world applications across industries reveals why extruded aluminum sizes and shapes have become so diverse.
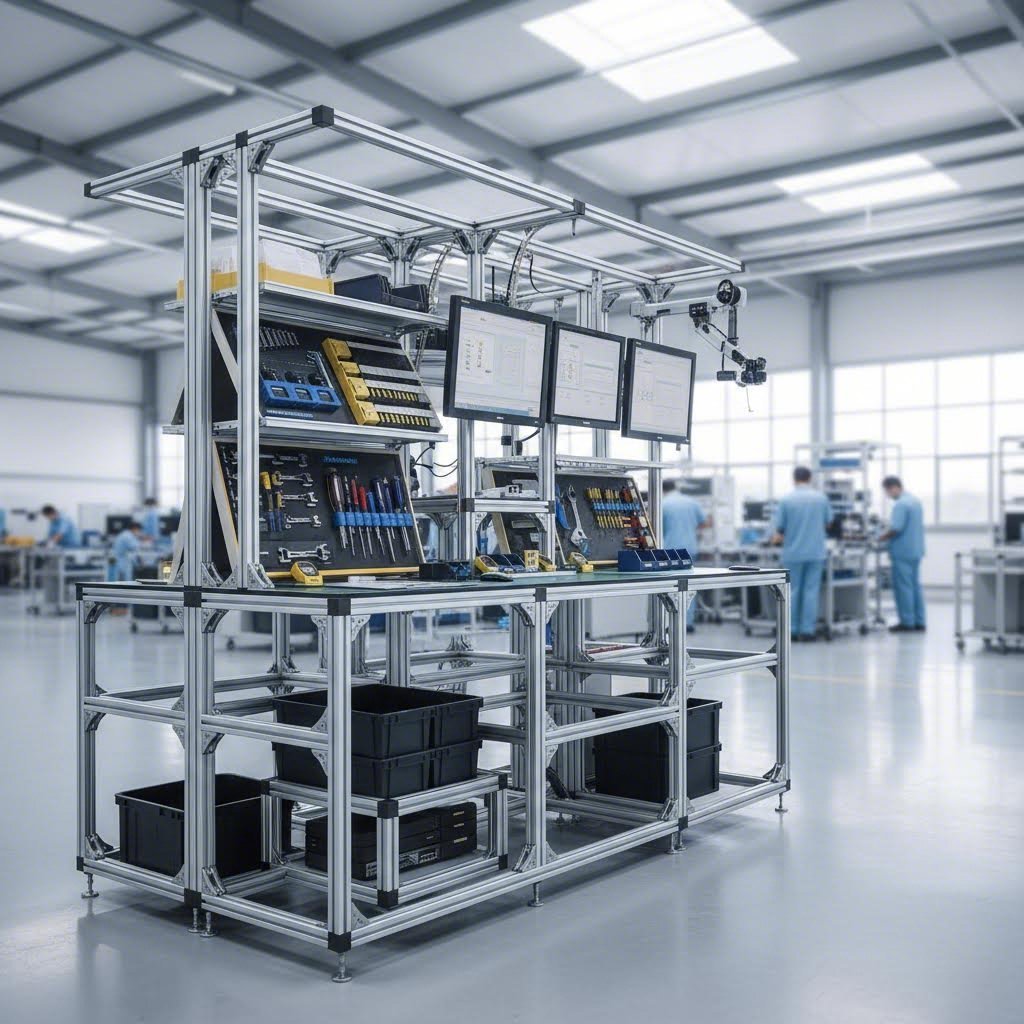
Now that you understand how to select the right profile, a natural question emerges: what are people actually building with these systems? The versatility of modular aluminum framing extends far beyond factory floors—though that's certainly where it shines brightest. Let's explore the practical applications that have made extruded aluminum framing the go-to solution across remarkably diverse industries.
Walk through any modern manufacturing facility, and you'll spot aluminum extrusion frame structures everywhere. The industrial sector embraced this technology decades ago, and adoption continues accelerating. Here's why these applications dominate:
Industrial applications represent just the beginning. Commercial and maker communities have discovered equally compelling uses for modular aluminum framing:
Why choose an extruded frame over traditional alternatives? Every material has strengths and limitations. Understanding these trade-offs helps you make informed decisions for your specific application:
| Property | Aluminum Extrusion | Steel (Welded) | Wood | Composite/Plastic |
|---|---|---|---|---|
| Weight | Low—approximately 1/3 of steel | High—densest option | Medium—varies by species | Low to Medium |
| Corrosion Resistance | Excellent—naturally forms protective oxide layer | Poor without treatment; stainless steel excellent but expensive | Poor—susceptible to rot and moisture damage | Excellent—immune to rust |
| Initial Cost | Medium to High | Low to Medium (can be half the cost of aluminum per industry sources) | Low | Medium |
| Ease of Modification | Excellent—reconfigure with basic tools | Poor—requires welding, grinding, refinishing | Moderate—requires carpentry skills | Poor—often requires replacement |
| Aesthetics | Clean, modern, professional appearance | Industrial; can be refined with powder coating | Warm, traditional | Varies widely by product |
| Precision/Straightness | Excellent—profiles perfectly straight from extrusion | Good—but can warp during welding | Variable—affected by moisture content | Good |
| Recyclability | 100% recyclable without quality loss | Highly recyclable | Biodegradable but limited reuse | Limited—often not recyclable |
| Assembly Speed | Fast—no special equipment needed | Slow—welding and finishing require time | Moderate | Fast with proper hardware |
When should you choose steel instead? According to industry guidance, steel fencing often makes sense for machine guarding where cost-effectiveness and faster installation outweigh reconfiguration needs. Steel's preassembled panels reduce installation time significantly, and the material handles heavy, rough handling better than aluminum. For constructions requiring maximum rigidity or where additional weight actually helps stability, steel remains the preferred option.
But when flexibility, precision, and long-term adaptability matter—prototype machines, evolving production lines, applications requiring frequent modification—aluminum structural framing delivers value that steel simply cannot match. The decision ultimately depends on whether your application values permanence or adaptability.
With applications understood and material comparisons clear, the next question becomes practical: how do all these components actually connect? The hardware that joins aluminum profiles together determines both the strength and the convenience of your modular system.
You've selected your profiles and understand the applications. But here's where projects succeed or fail: the connections. Those T-slots running along every profile are useless without the right hardware to join them together. Let's demystify the fastening options that suppliers like 80/20 mention but rarely explain in practical terms.
Think of connection hardware as the vocabulary of modular framing. Just as different words serve different purposes, each fastener type addresses specific structural and aesthetic needs. Choosing incorrectly doesn't just affect appearance—it can compromise your entire structure's integrity.
The sheer variety can feel overwhelming. According to 80/20's fastener guide, the simplest way to categorize options is dividing them into internal and external fasteners. Internal fasteners are machined into the profiles themselves, creating strong bonds with fewer visible parts. External fasteners mount on the outside, offering easier implementation and more configuration flexibility.
Here's a practical comparison of the most common connection types you'll encounter:
| Connection Type | Visibility | Strength | Ease of Assembly | Reconfigurability | Best Applications |
|---|---|---|---|---|---|
| T-Nuts and Bolts | Partially visible | Moderate to High | Easy | Excellent | General connections, adjustable mounting, accessory attachment |
| Corner Brackets (L Shaped Brackets) | Visible | Good | Very Easy | Excellent | Quick assembly, right-angle joints, accessible connections |
| Anchor Fasteners | Hidden | High | Moderate | Good | Clean aesthetics, permanent frames, customer-facing structures |
| Gussets | Visible | Maximum | Easy | Good | Heavy loads, structural reinforcement, 45-degree supports |
| 4x4 Brackets/4x4 Post Brackets | Visible | High | Very Easy | Excellent | Large profile connections, heavy-duty frames, base mounting |
So when does each method make sense? The decision comes down to three factors: load requirements, aesthetic preferences, and how often you'll need to reconfigure.
T-Nuts and Bolts represent the foundation of T-slot assembly. A T-nut slides into the channel, rotates to lock in place, and a bolt through your bracket or component tightens everything together. This method offers infinite positioning along the profile length—mount that sensor anywhere, shift it 5mm tomorrow if needed. For general connections and component mounting, you'll use these constantly.
Corner Brackets and L Shaped Brackets create quick 90-degree connections visible on the profile exterior. They require no machining, install in seconds, and allow easy adjustment. The trade-off? They're visible. For industrial applications where function trumps form, this matters little. For customer-facing displays, you might prefer hidden alternatives. According to CPI Automation, corner brackets are indispensable for creating stable, square corners in shelving and workbench applications.
Anchor Fasteners deliver the clean aesthetics many applications demand. Comprising a socket head cap screw, cam, and T-nut, these internal fasteners create hidden connections completely recessed within the profiles. They're one of the strongest internal fastening methods according to industry sources, offering long-lasting connections. The catch? Assembly requires more precision and pre-planning since connections aren't visible during tightening.
Gussets are your heavy-duty reinforcement option. These angular plates strengthen connection points beyond what simple brackets achieve. When building frames that support significant weight—think machine bases, overhead structures, or anything where failure isn't acceptable—gussets provide the maximum rigidity. A 45-degree gusset supporting a 90-degree joint dramatically increases resistance to racking forces.
Here's where many DIY builders go wrong: under-tightening or over-tightening fasteners. Both create problems.
Under-tightened connections work loose over time, especially under vibration. Bolts for 4x4 posts and similar heavy-duty fasteners need proper torque to develop full clamping force. Without it, your frame gradually loosens—you'll notice increasing play at joints that seemed solid initially.
Over-tightening strips threads—particularly in softer aluminum—or cracks plastic components like end caps. Once threads strip, that connection point becomes useless without repair inserts or replacement profiles.
Most T-slot hardware specifies recommended torque values. A general guideline for common M6 fasteners in aluminum profiles: 8-10 Nm provides secure clamping without thread damage. Larger fasteners (M8, M10) require proportionally higher torque. When in doubt, refer to manufacturer specifications or consult a screw dimensions chart for your specific hardware.
Thread engagement matters equally. Bolts should engage at least 1.5 times their diameter into the mating component—more for safety-critical connections. A 6mm bolt needs at least 9mm of thread engagement for reliable strength. Shallow engagement concentrates stress on fewer threads, inviting failure under load.
Beyond basic connections, specialty hardware transforms simple frames into functional systems:
Running short mid-project frustrates everyone. Running a separate order for three missing T-nuts wastes time and shipping costs. Here's a practical approach to estimation:
Count your joints: Every connection where two profiles meet needs fasteners. A simple rectangular frame has four corner joints. Add cross-members, and each intersection adds another connection point. Sketch your design and count methodically.
Plan for accessories: Every bracket, panel clip, hinge, or mounted component needs its own fasteners. That workbench with twelve accessory mounting points needs twelve T-nut sets beyond the frame connections.
Add contingency: Order 10-15% extra hardware. Dropped T-nuts disappear. Occasional over-tightening strips threads. Having spares on hand beats waiting for replacements.
Consider future modifications: If your project will evolve—adding shelves, repositioning equipment, expanding the structure—order hardware for anticipated changes now. Matching hardware from the same supplier ensures compatibility.
Don't forget end caps and covers: These finishing components often get overlooked until final assembly reveals every open profile end. Count your profile cuts and order accordingly.
With the right connection hardware selected and quantities estimated, your aluminum frame assembly becomes straightforward. But appearance matters too—and that's where surface treatments enter the picture, protecting your investment while enhancing visual appeal.
Your aluminum frame is assembled, connections are solid, and the structure performs exactly as designed. But here's the question many builders overlook until it's too late: what happens when that raw aluminum meets the real world? Surface treatments transform functional profiles into finished products—protecting against environmental damage while delivering the appearance your application demands.
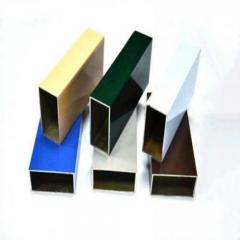
Every aluminium extrusion profile leaves the die with what manufacturers call a "mill finish"—the natural state of aluminum after extrusion. This surface shows die marks, minor oxidation, and inconsistent appearance. For hidden structural components, mill finish works fine. For anything else? You'll want to consider your options carefully.
According to Gabrian International, while aluminum's excellent properties make it a regular choice for extrusion designers, the right surface finish can elevate products from "good" to "outstanding." Surface finishes improve corrosion resistance, wear resistance, and aesthetic appearance to make extrusions last longer and look better.
Here's what's available:
Choosing the right treatment isn't about picking the "best" option—it's about matching protection level to actual environmental exposure. Over-specifying wastes money; under-specifying leads to premature degradation.
| Environment | Recommended Treatment | Why It Works |
|---|---|---|
| Indoor, climate-controlled | Mill finish or clear anodizing | Minimal exposure; basic protection sufficient |
| Indoor, visible/customer-facing | Colored anodizing or powder coating | Aesthetic requirements justify additional cost |
| Outdoor, moderate climate | Powder coating | UV resistance and color retention over years |
| Outdoor, coastal or industrial | PVDF coating | Maximum chemical and salt spray resistance |
| Food processing or cleanroom | Anodizing (clear or specific colors) | Non-porous, easy to clean, won't contaminate |
| High-wear mechanical applications | Hard anodizing | Thicker oxide layer resists abrasion |
For anodized aluminum extrusions specifically, the treatment creates a surface that's actually harder than the base aluminum. This integral protection won't chip or peel like applied coatings can—the oxide layer is part of the metal itself. That's why anodizing remains preferred for applications where tight dimensional margins and outstanding corrosion resistance matter most.
Here's something suppliers rarely mention: surface treatments add thickness. That extra material—however slight—affects how hardware fits within T-slots.
Anodizing adds roughly 0.025mm per surface for standard processes. Powder coating adds considerably more—typically 0.05-0.1mm. In most applications, this doesn't matter. But for precision fits or when using hardware at the tight end of tolerance ranges, that added thickness can create assembly challenges.
Practical considerations:
Every surface treatment adds cost—sometimes substantially. When does that investment make sense?
Outdoor installations: Without proper protection, aluminum corrodes in outdoor environments. The white, powdery oxidation that develops on unprotected extruded aluminum tube isn't just unsightly—it weakens the material over time. PVDF or quality powder coating pays for itself in extended service life.
Corrosive environments: Chemical plants, food processing facilities, marine applications, and swimming pool equipment all demand enhanced protection. The cost of premium finishes pales against replacement costs when standard treatments fail prematurely.
Customer-facing applications: Retail displays, trade show booths, office furniture, and architectural installations need to look professional. That black aluminum extrusion framing your product display represents your brand. Investing in quality finishes communicates quality products.
High-wear surfaces: Machine frames, conveyor systems, and equipment handles see constant contact. Hard anodizing provides abrasion resistance that standard treatments cannot match.
For projects requiring comprehensive surface treatment options, manufacturers offering end-to-end processing services simplify procurement significantly. Shengxin Aluminium's processing services, for example, provide custom anodizing in specialty colors like Champagne and Rose Gold, along with powder coating, PVDF, and micro-arc oxidation—all integrated with their extrusion capabilities. This single-source approach ensures finish specifications align perfectly with profile tolerances, eliminating the coordination headaches of managing separate extrusion and finishing vendors.
With surface treatment options understood, the final consideration becomes equally practical: where do you actually source quality alu extrusion profile components? The supplier you choose affects everything from lead times to technical support—and ultimately, project success.
You've designed your frame, selected your profiles, and specified the perfect surface finish. Now comes the question that determines whether your project succeeds on schedule and budget: where to buy aluminum extrusion profiles that meet your exact requirements? The supplier landscape ranges from local distributors stocking standard shapes to global manufacturers offering complete custom extrusion services. Navigating these options strategically can save thousands of dollars and weeks of lead time.
Not all aluminum extrusion supply sources are created equal. According to industry analysis for 2025, buyers should evaluate vendors across multiple dimensions: product quality, technological capabilities, customization flexibility, pricing, delivery reliability, sustainability practices, and customer support. But how do these criteria translate into practical decision-making?
Here's a systematic framework for evaluating potential suppliers:
Your sourcing strategy should evolve with your project phase. Prototype development demands flexibility and speed—you're iterating designs, testing concepts, and likely ordering small quantities. Production runs prioritize cost efficiency, quality consistency, and reliable supply. Few suppliers excel at both extremes.
For prototyping, consider:
For production volumes, prioritize:
According to Paramount Extrusions, the question of where to buy aluminum extrusions doesn't have a one-size-fits-all answer—it comes down to balancing cost, lead time, and performance. Understanding when to choose domestic versus import sources, and custom versus stock profiles, sets your project up for success.
Standard catalog profiles cover an enormous range of applications. Before investing in custom tooling, honestly assess whether existing shapes meet your needs. The aluminum extrusion industry has developed standard profiles specifically because they solve common engineering problems efficiently.
Choose catalog profiles when:
Invest in custom extrusions when:
Custom die costs vary widely—from a few hundred dollars for simple shapes to several thousand for complex multi-cavity dies. Amortized across production volume, this investment often pays back quickly. A custom profile that eliminates secondary machining operations or consolidates multiple components can actually reduce total cost despite higher per-foot pricing.
The most efficient sourcing relationships come from suppliers offering complete solutions: die development, extrusion, secondary processing, surface treatment, and logistics. This integration eliminates the coordination burden of managing separate vendors for each production step.
Consider what happens without integration: you order extruded aluminum for sale from one supplier, ship to a machine shop for cutting and drilling, transfer to an anodizer for finishing, and finally receive components. Each handoff introduces delays, potential damage, quality variability, and communication gaps. Problems become finger-pointing exercises between vendors.
Integrated suppliers own the entire process. When specifications require adjustment, one conversation addresses all production steps. Quality issues trace directly to their source. Lead times compress because material doesn't wait between separate operations. And pricing reflects actual production efficiency rather than margin stacking across multiple vendors.
For those seeking this comprehensive approach, Shengxin Aluminium exemplifies the integrated service model. With over 30 years of industry experience, their facility houses 35 extrusion presses ranging from 600T to 5500T capacity—enabling production of everything from delicate architectural profiles to heavy industrial sections. Their CNC machining centers handle precise cutting, drilling, and bending to exact specifications, while comprehensive surface treatment options including custom anodizing colors, powder coating, PVDF, and micro-arc oxidation complete the offering. Their technical team provides end-to-end support from die development through mass production, making them a strong option for buyers seeking factory-direct custom extrusion services.
Geographic sourcing decisions balance cost against lead time, quality assurance, and communication convenience. Both approaches have legitimate applications.
Domestic sourcing advantages:
Import sourcing advantages:
Per Paramount Extrusions' guidance, imported extrusions often cost 20-40% less than domestic equivalents—but require longer planning horizons and larger order quantities to be practical. For ongoing production programs where demand is predictable, import sourcing delivers compelling economics. For prototype work, emergency requirements, or variable-demand situations, domestic suppliers provide essential flexibility.
Many successful procurement strategies blend both approaches: domestic sources for development work and urgent needs, transitioning to import sources once designs stabilize and volumes justify ocean freight economics.
The aluminum extrusion industry continues evolving, with sustainability practices, automation investments, and consolidated supply chains reshaping the competitive landscape. According to 2025 industry analysis, companies investing in eco-friendly processes and advanced automation will gain competitive advantages. Strategic partnerships between buyers and integrated suppliers—rather than purely transactional relationships—increasingly differentiate successful projects from troubled ones.
Whether you're sourcing a dozen profiles for a prototype workstation or tens of thousands of feet for production equipment, applying these evaluation criteria systematically leads to supplier relationships that support your project's success—not just this time, but for the modular, reconfigurable applications that aluminum frame extrusion profiles enable.
T-slot aluminum extrusion features T-shaped channels running along the profile length that accept specialized hardware like T-nuts and brackets. When a T-nut slides into the channel and rotates 90 degrees, it locks in place, allowing connections at any point without drilling or welding. This design enables infinite adjustability, easy reconfiguration, and tool-free assembly using basic wrenches and Allen keys.
Series numbers typically correspond to the profile's outer dimension in millimeters. A 40 Series profile measures 40x40mm, while a 20 Series measures 20x20mm. The series also determines slot width—larger series have wider slots accepting heavier-duty fasteners. The 4040 designation is the industrial workhorse, balancing structural capability with cost-effectiveness for machine frames and workstations.
Choose 6063 aluminum for most applications—it offers excellent extrudability, superior surface finish, and outstanding anodizing response at lower cost. Select 6061 when structural strength is critical, as it delivers approximately 50% higher tensile strength. For general modular framing like workstations and enclosures, 6063 performs perfectly; reserve 6061 for heavy loads or safety-critical components.
Evaluate suppliers based on profile variety, custom extrusion capabilities, secondary processing services (cutting, drilling, machining), surface treatment options, and technical support. Integrated manufacturers like Shengxin Aluminium offer complete solutions from die development through finishing, eliminating coordination headaches. For prototypes, choose distributors with low minimums; for production, prioritize factory-direct relationships with comprehensive processing capabilities.
Common treatments include mill finish (economical, indoor only), clear anodizing (corrosion protection, maintains metallic look), colored anodizing (branding, identification), powder coating (maximum durability, unlimited colors), and PVDF coating for extreme environments. Anodizing creates a surface harder than base aluminum that won't peel, while powder coating excels for outdoor applications requiring UV resistance and vibrant colors.


 บริการออนไลน์
 0086 136 3563 2360
 sales@sxalu.com
 +86 136 3563 2360
 ไทย
 English
 français
 Deutsch
 русский
 español
 português
 العربية
 Việt
 Українська